




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Avoiding Misleading Rectangular Clinching Tool Sample Results: A Technical Validation Guide
Why Prototype Results Can Be Deceptive in Sheet Metal Clinching
Evaluating sample joints produced by a rectangular clinching tool requires understanding how press force, die geometry, and sheet metal properties interact. Laboratory samples frequently yield optimistic joining results because test coupons feature uniform thickness, clean surfaces, and ideal ambient conditions. In real manufacturing environments—such as stainless steel commercial kitchen fabrication, commercial freezers, and control cabinet production lines—variations in metal temper, protective oil films, and minor gauge tolerances alter how the metal flows into the rectangular die matrix.
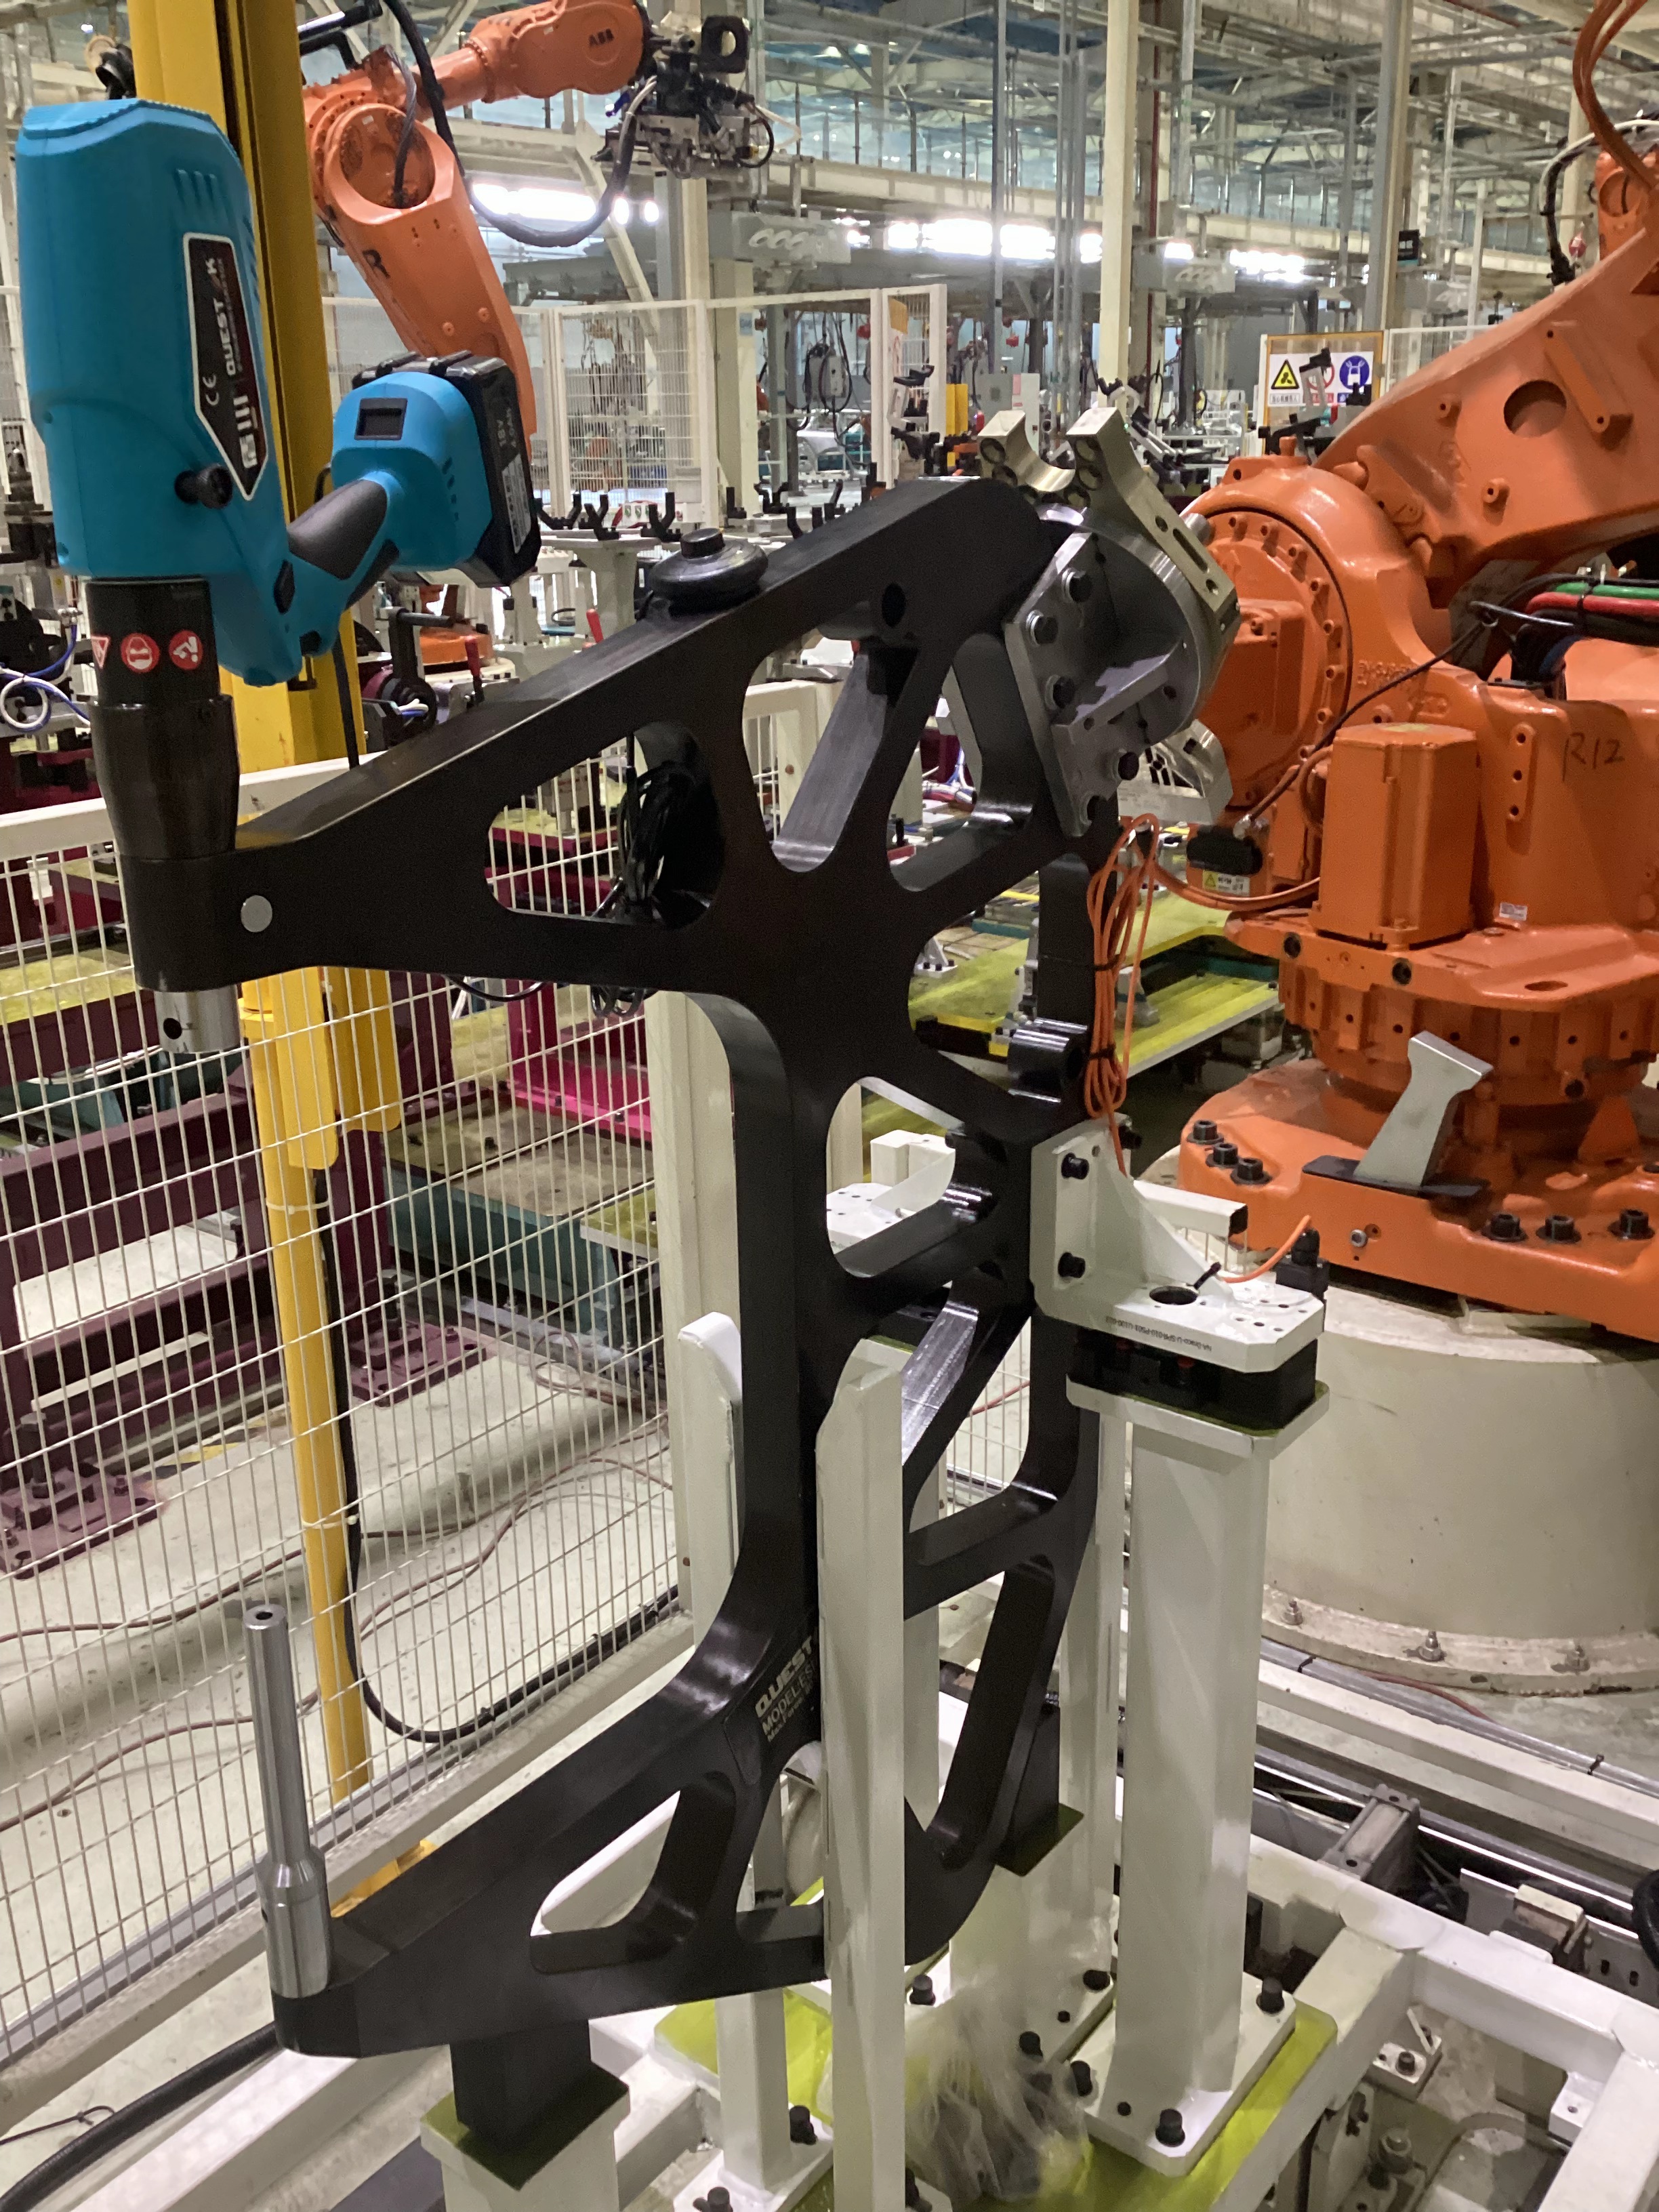
To avoid misinterpreting prototype success, engineering teams must evaluate force displacement curves during joint formation. Rectangular clinching equipment relies on controlled stroke depth to form an interlocking joint without piercing the sheet metal. If the output pressure is improperly calibrated—such as failing to adjust within an adjustable 1 to 80 kN operating range—the sample may appear intact visually while lacking the required undercut dimension for structural load stability.
Key Solutions for Reliable Tooling Validation
- Validate multi-material sheet metal joints under exact production tolerances rather than relying on ideal single-sheet lab samples.
- Verify single-step joint execution on pre-painted or coated stainless steel to confirm surface finish remains intact without secondary polishing or repainting.
- Perform destructive shear and pull-out tests across high-volume production batches to eliminate variance caused by die wear or improper pressure calibration.
- Inspect rectangular clinching joint cross-sections to verify mechanical interlocks before deploying equipment to automated assembly lines, such as HVAC ducting, white goods, and control cabinet systems.
Factory Line Performance & Structural Integrity Verification
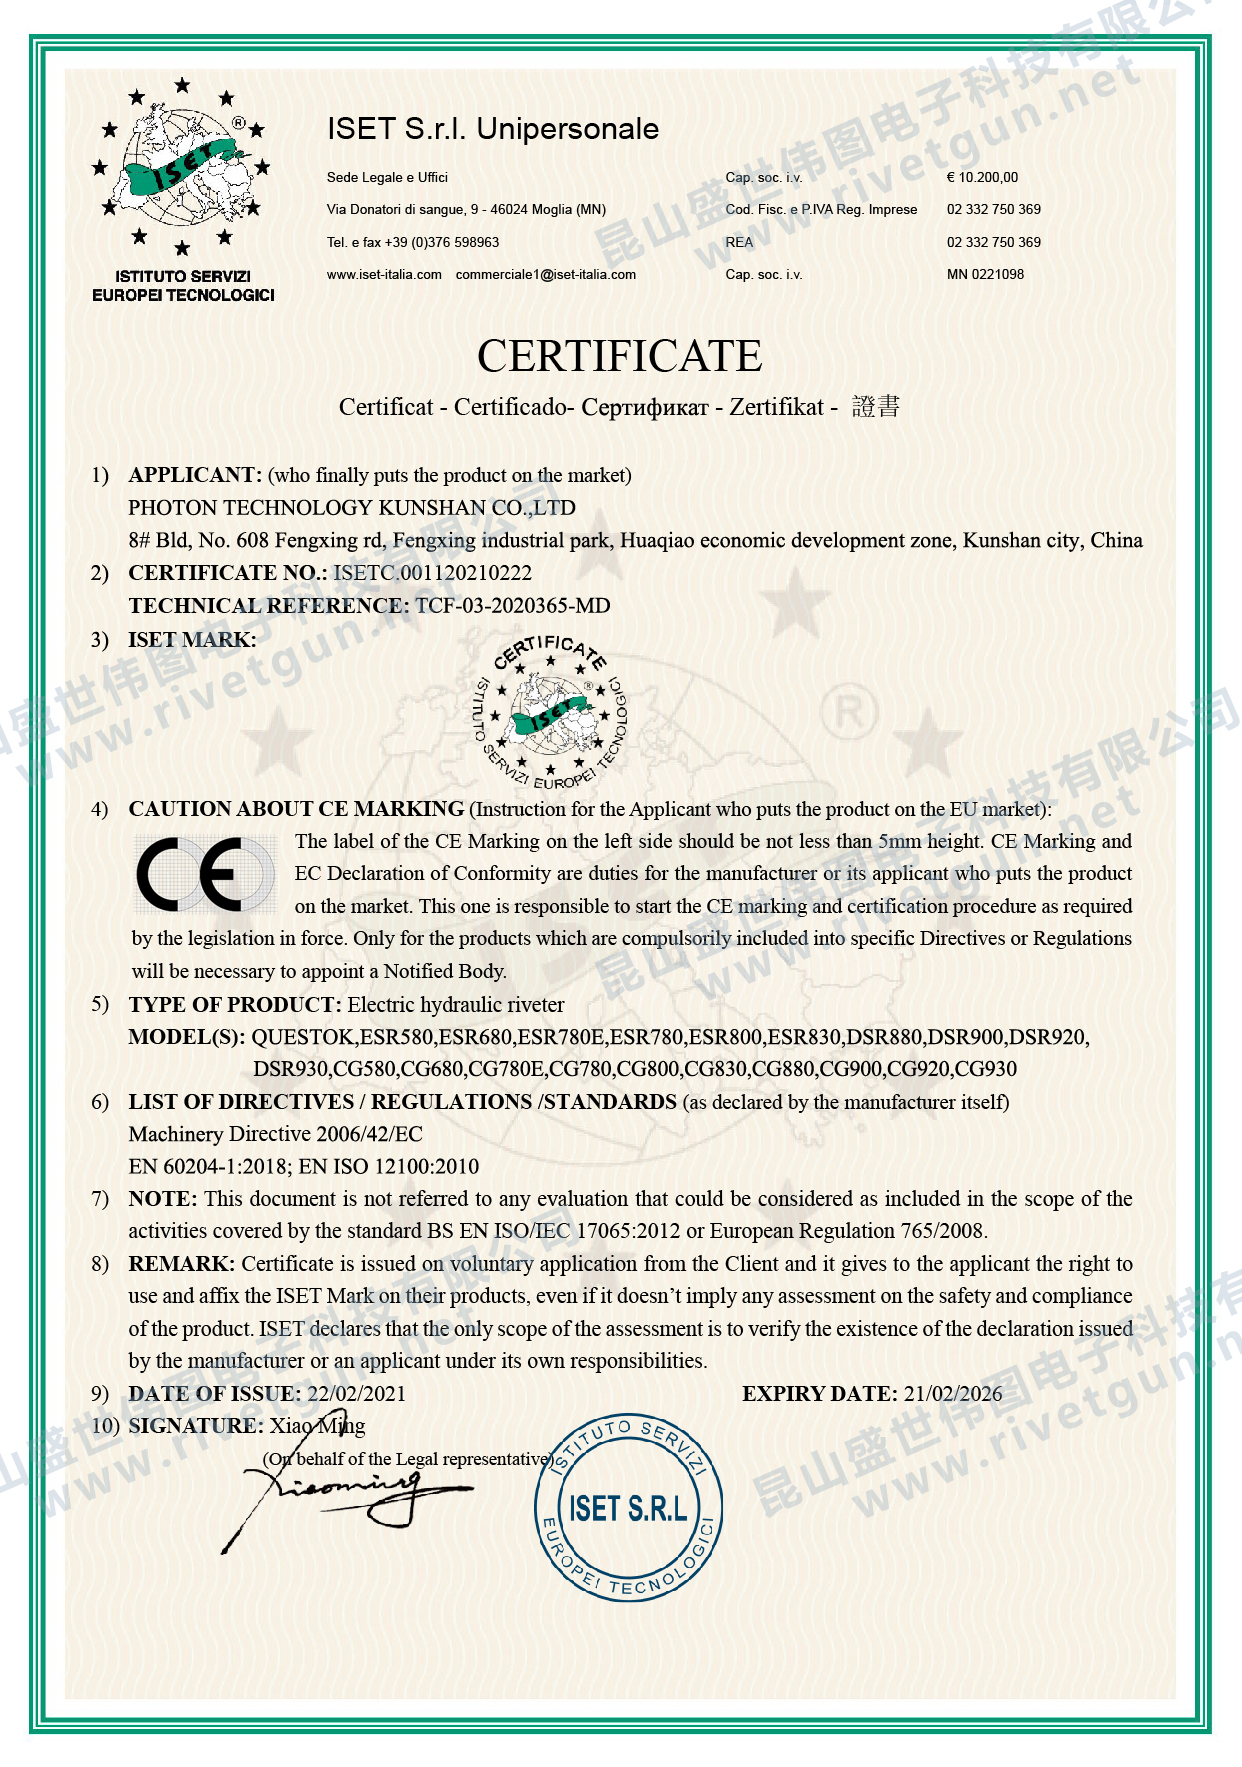
Field data from automated enclosure production, including Midea control cabinet assembly lines, demonstrates that transitioning from traditional spot welding to single-step clinching eliminates consumable costs while maintaining joint integrity. However, validation protocols must incorporate cross-sectional metallographic analysis to confirm joint neck thickness and interlock value across consecutive cycles. Equipment validated under CE certified standards, including certificates ISETC.001120210222 and 3N210218.PTK0S25, ensures operational safety and repeatable force delivery across production shifts.
Data & Method Comparison
| Parameter / Metric | Rectangular Clinching Tool | Resistance Spot Welding | Standard Riveting System |
|---|---|---|---|
| Process Execution | Single-step, cold-forming operation | Multi-stage thermal melting | Multi-stage insertion and setting |
| Consumable Requirement | None (rivetless joining) | Electrodes and gas shield | External rivets required |
| Surface Post-Processing | No polishing or repainting needed | Grinding and thermal cleanup required | Minor surface flush adjustments |
| Coating Integrity | Preserves galvanized and painted layers | Burns surface protective layers | Pierces protective coatings |
| Quality Verification Method | Button height & cross-section check | Destructive nugget tear test | Rivet head setting inspection |
Frequently Asked Questions
Why do laboratory clinching samples show higher strength than mass production joints?
Laboratory samples are created under static pressing speeds with hand-selected material coupons. Mass production introduces thermal expansion in tooling, high-cycle vibration, and thickness tolerances across sheet metal coils, which reduce joint interlock depth if hydraulic pressure is not precisely regulated.
What non-destructive test confirms a rectangular clinching joint is reliable?
Measuring the residual bottom thickness of the clinching button with a digital anvil micrometer provides an immediate non-destructive indication of proper force delivery and die fill during production runs.
Can rectangular clinching tools join dissimilar sheet metals without surface damage?
Yes. Rectangular clinching forms a cold-pressed mechanical joint between dissimilar metals, such as aluminum and galvanized steel, without heat affected zones, surface discoloration, or the need for post-process painting.
Conclusion & Best Practices
To eliminate misleading sample evaluation results, engineering teams must validate rectangular clinching equipment using production-grade sheet metal batches, dynamic cycle speeds, and strict cross-sectional measurement standards. Full functional testing across standard and customized tooling configurations ensures joint consistency in HVAC, kitchen equipment, and vehicle sub-assembly lines. Operational deployment benefits from selecting equipment subject to 100% pre-delivery inspection and clear troubleshooting guidelines supported by direct factory technical service. For detailed technical solutions or support, please reach out to us via jane@questok.com.
About Us
PHOTON TECHNOLOGY KUNSHAN CO.,LTD is an industrial technology company established in 2011, operating a 5000 sqm manufacturing facility with a team of 20-50 employees. The company specializes in developing advanced joining and fastening technologies, including battery-powered hydraulic riveting tools, self-piercing riveting systems, clinching guns, and fasteners pressing tools. Holding CE certifications, the enterprise provides equipment to automotive, HVAC, electronic, and general sheet metal fabrication industries worldwide.
REPORT