




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How Industrial Profile Tolerances Influence Assembly Accuracy and Product Quality
Industrial aluminium profile tolerances play an important role in assembly precision, structural performance, and the appearance of the completed product. Key factors include cross-section dimensions, interface geometry, wall-thickness consistency, straightness, twisting, surface waviness, and coating quality. Because the available product information does not specify numerical tolerance limits, the required values should be confirmed through the approved technical drawing, alloy and temper requirements, inspection records, and the intended application, including automation frames, heat sinks, doors, and windows.
Key Factors for Reliable Profile Assembly
- Accurate cross-section and interface dimensions help connected components align and fasten correctly.
- Consistent wall thickness supports predictable strength, connection performance, and visual uniformity.
- Controlled straightness, twisting, and waviness help maintain frame squareness and prevent visible defects.
- Appropriate surface treatment protects the finished profile and improves colour and coating consistency.
- Material and temper conformity ensures that the profile performs as specified in the approved design.
How Tolerance Control Affects Industrial Applications
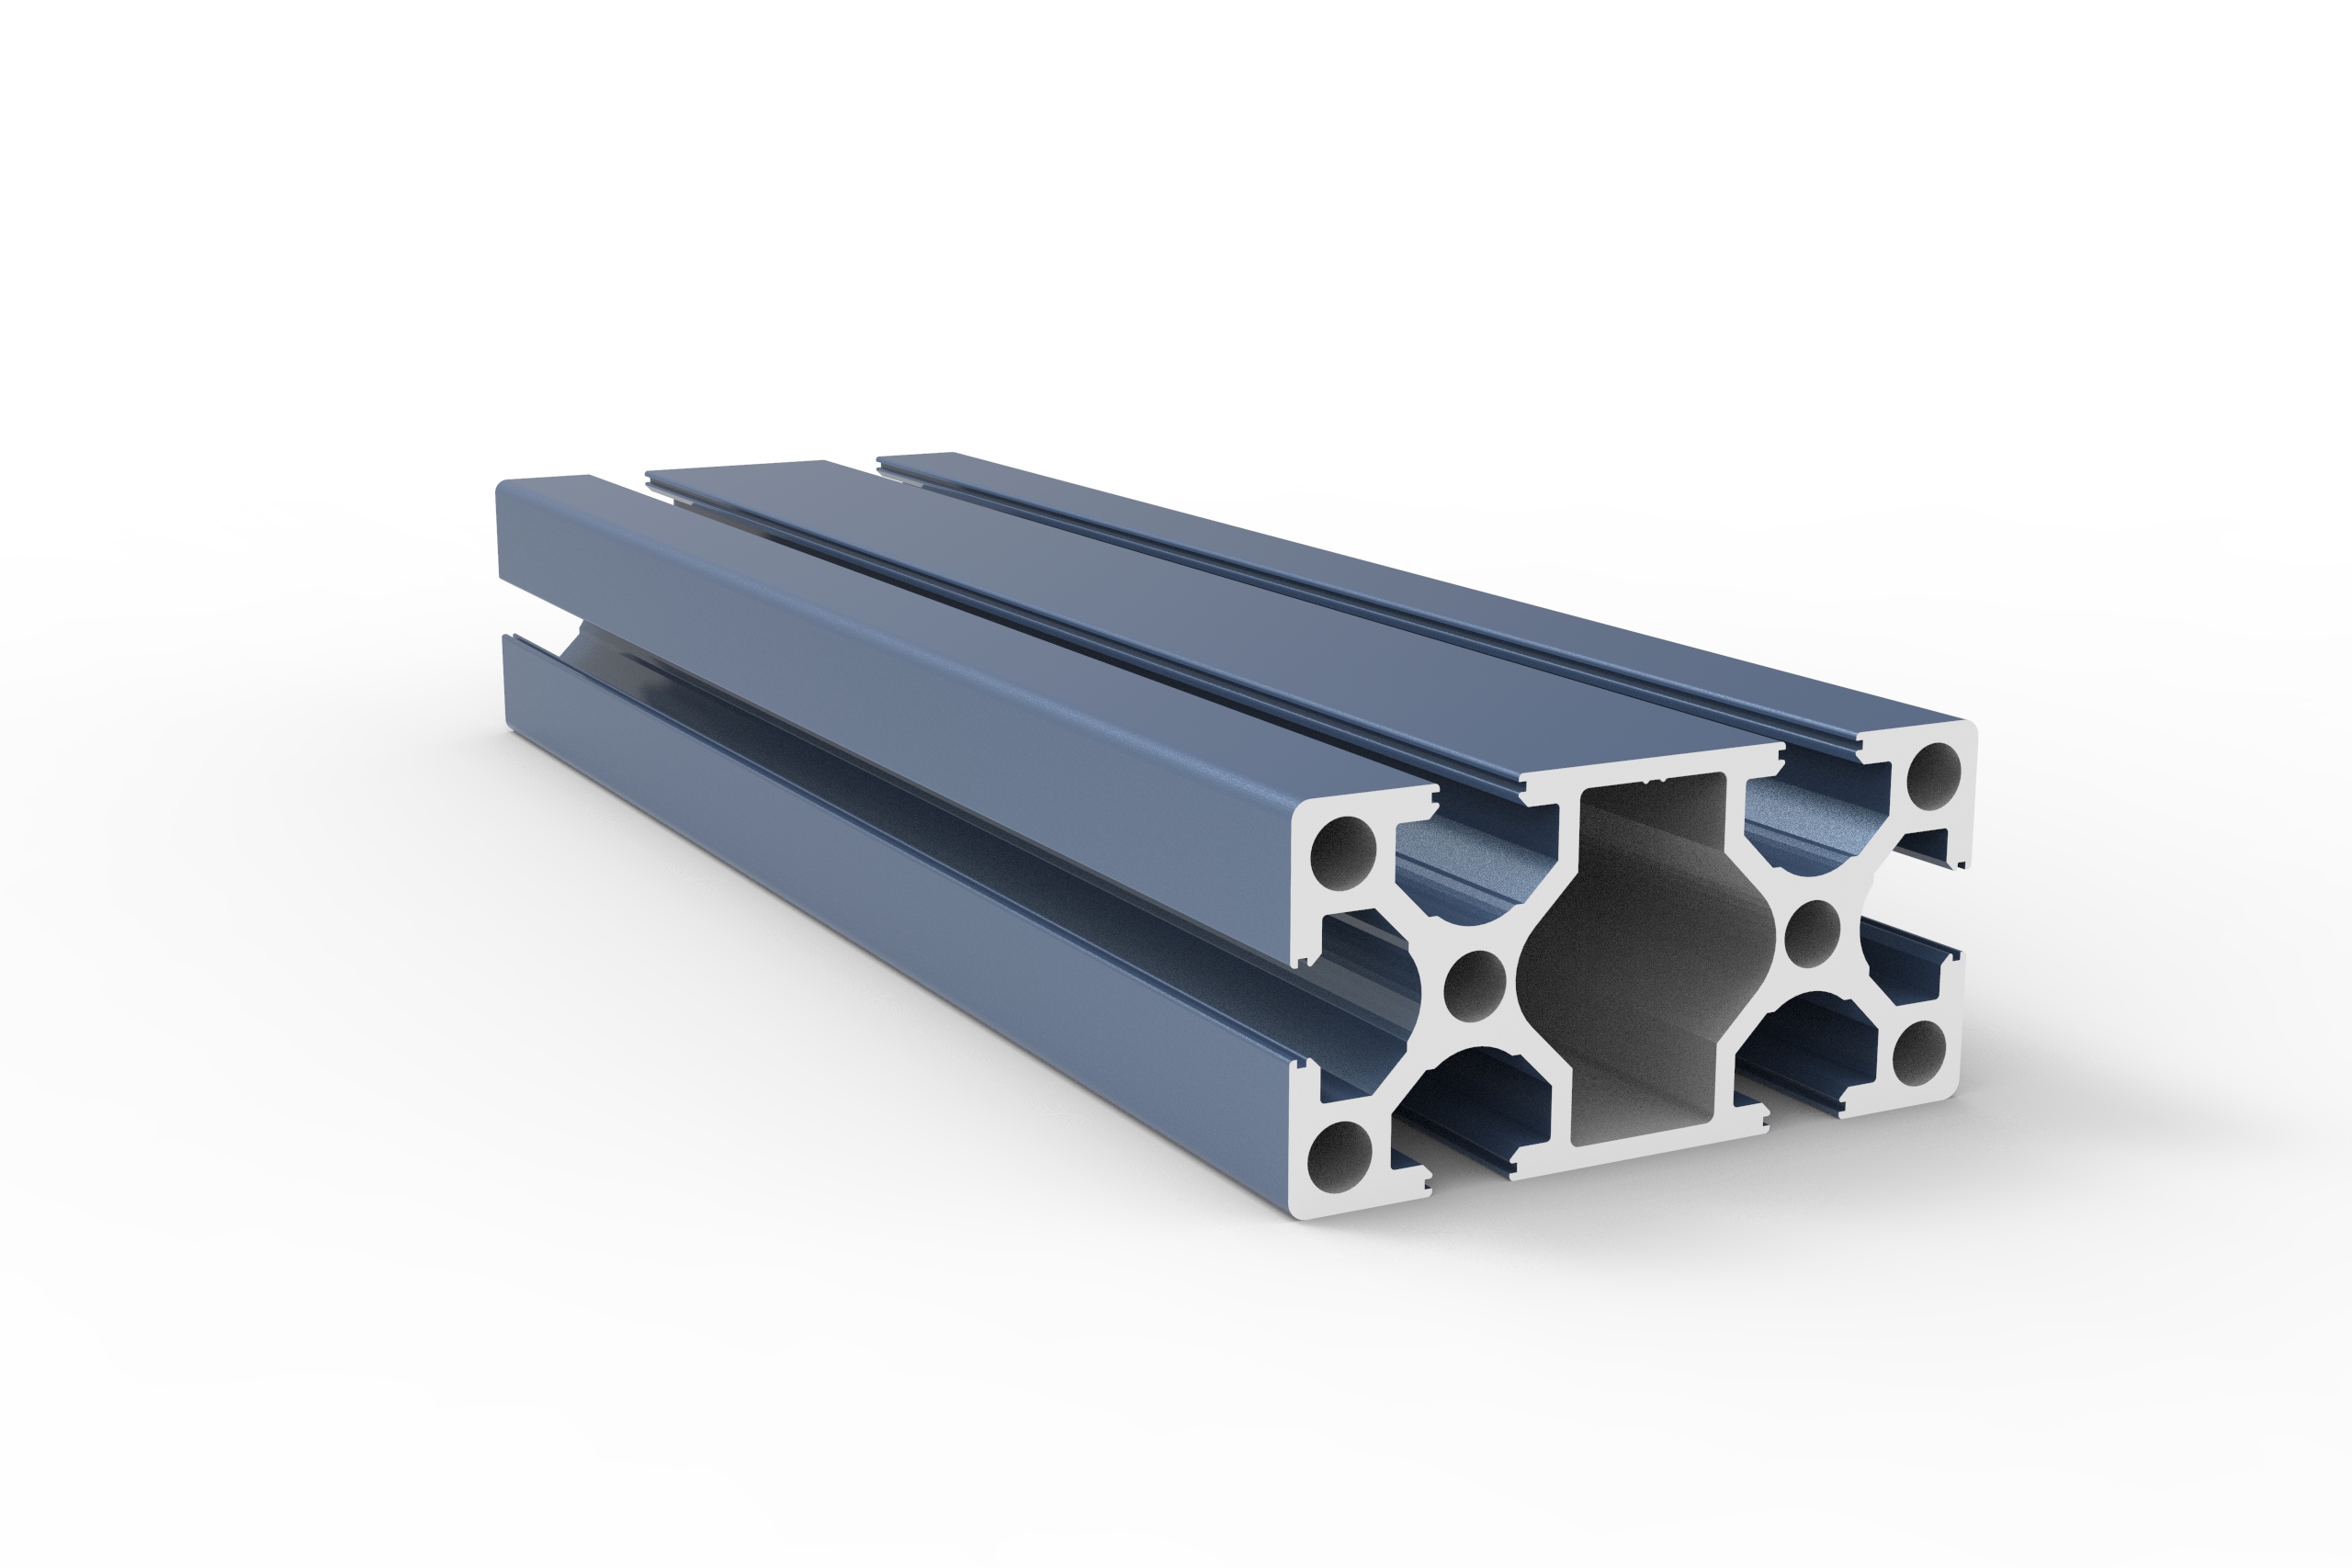
The accuracy of an extruded profile depends on how closely the manufactured section matches its design. Differences in width, height, slot position, corner radius, or other connection dimensions may cause gaps, offset joints, uneven surfaces, or additional adjustment during installation. Xinhe Aluminium identifies alloys including 6063, 6060, 6061, 6463, 6005, 6082, and 6106, with T5 and T6 tempers. However, the supplied product data does not state numerical dimensional tolerances. The applicable limits should therefore be taken from the approved profile drawing, purchase contract, or project specification.
Wall Thickness and Structural Consistency
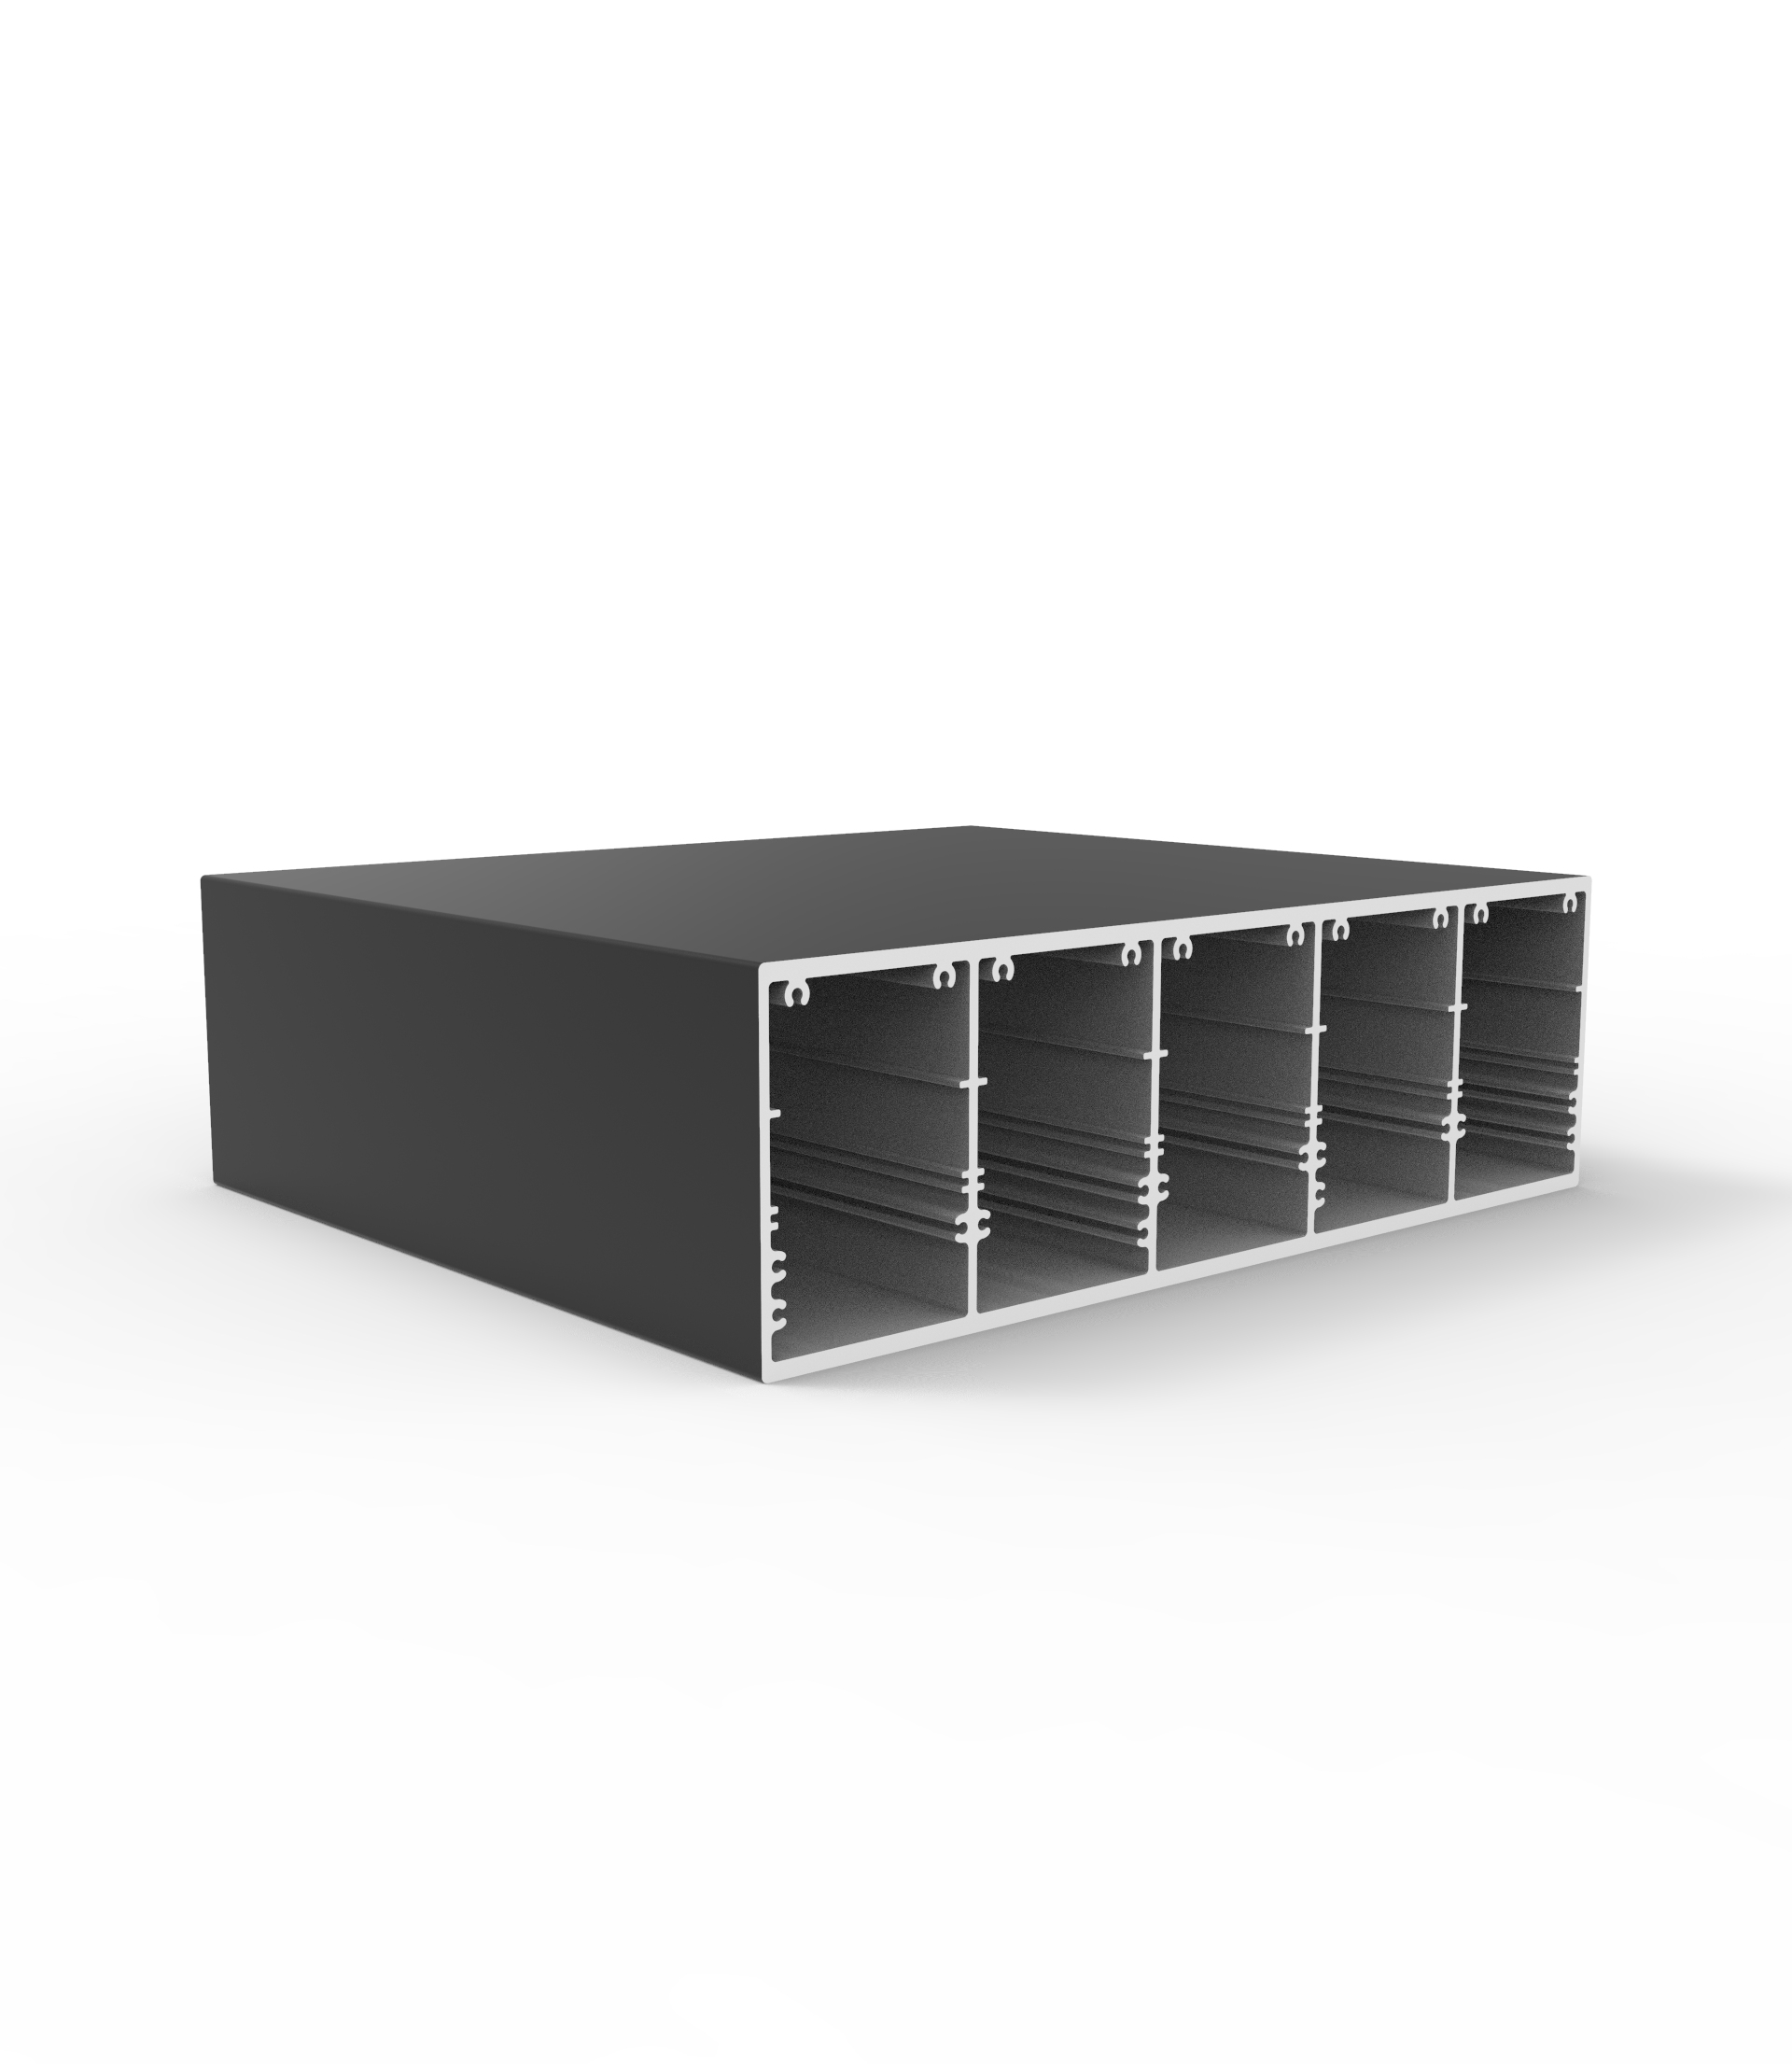
Wall-thickness conformity influences the consistency of fastened connections, the perceived strength of the finished assembly, and the profile's response to operating loads. A cooperation record for a high-rise office building describes the use of solid virgin 6063-T5 aluminium alloy and standard wall thickness. This is project-specific customer feedback rather than a published numerical tolerance range, so formal acceptance should still be based on the relevant technical documentation.
Form Accuracy: Straightness, Twist, and Waviness
Long profiles must remain sufficiently straight and stable to seat evenly in frames and connect without forced correction. Bending, twisting, or wavy deformation can affect frame squareness, create uneven joints, and reduce the visual quality of the completed structure. In a residential building cooperation record, the customer reported profiles with straightness and without bending, twisting, or wavy deformation. The statement reflects the reported project result but does not establish a measured tolerance value.
Surface Finish and Coating Performance
Surface quality should be evaluated separately from dimensional accuracy. Powder-coating uniformity, colour matching, adhesion, resistance to peeling, and resistance to fading all contribute to the final appearance and service life. Xinhe Aluminium lists Qualicoat certification for powder coating in Europe and an SGS substrate material quality inspection certificate. These credentials support the company's stated quality framework, while each project should still define its own coating and colour acceptance requirements.

Inspection Approach for Tolerance Compliance
A practical inspection program should begin by comparing the extruded section with the approved drawing and confirming the specified raw material before production. Finished profiles should then be checked for dimensional accuracy, wall thickness, straightness, twisting, surface condition, and material or temper conformity before they enter assembly. The stated quality system includes 100% production-line inspection, laboratory sampling and testing, and incoming raw-material inspection. The company also identifies a CNAS-accredited national laboratory as part of its testing capability.
Comparison of Main Quality Factors
| Quality factor | Impact on assembly and finished product | Recommended verification |
|---|---|---|
| Cross-section and interface dimensions | Incorrect dimensions may cause gaps, misalignment, difficult fastening, or inconsistent joints. | Check against the approved drawing because numerical values are not provided in the product data. |
| Wall-thickness consistency | Variation may affect structural behavior, connection feel, and visual uniformity. | Confirm the specified wall thickness and inspect representative production samples. |
| Straightness, twisting, and waviness | Deformation can lead to uneven seating, frame distortion, and visible assembly defects. | Use project inspection requirements; customer feedback reports straight profiles without these defects. |
| Coating and colour consistency | Surface variation can result in peeling, fading, colour differences, or a lower-quality appearance. | Assess coating performance and colour against the project acceptance criteria; Qualicoat certification is listed. |
| Alloy and temper conformity | Incorrect material selection can change processing behavior and service performance. | Verify the specified alloy and T5 or T6 temper through incoming-material and production records. |
Frequently Asked Questions
Does the available information include numerical profile tolerances?
No. The supplied information lists alloys, tempers, minimum order quantity, delivery time, export markets, and inspection stages, but it does not provide numerical limits for dimensions, straightness, twisting, or wall thickness.
Which characteristics have the greatest effect on assembly accuracy?
Cross-section dimensions, interface locations, wall-thickness consistency, straightness, twisting, and waviness directly influence mating accuracy, fastening, frame alignment, and joint uniformity.
How should finished profile quality be assessed?
Use the approved drawing and contract requirements as the primary reference. Combine dimensional and geometric inspection with incoming-material checks, production-line inspection, laboratory testing, and a separate review of coating and colour quality.
Conclusion and Procurement Recommendations
When purchasing industrial aluminium profiles, define dimensional, geometric, wall-thickness, material, and surface-quality requirements before production begins. Since the available product information does not state numerical tolerance limits, these values must be included in the approved drawing or contract. Xinhe Aluminium states a 3-ton MOQ and a 15-20 day delivery period, supported by production-line inspection, laboratory testing, and incoming-material inspection. The company also provides full industrial-chain, distribution, and direct-sales services. For technical support or a project-specific solution, contact xh@xinhealuminium.com.
About Xinhe Aluminium
Guangdong Xinhe Aluminium Co., Ltd specializes in the research, development, and manufacture of architectural, decorative, and industrial aluminium profiles. Founded in 1998, the company operates across 666,670 square metres and reports 60 modern extrusion production lines with capacities ranging from 1,100 to 5,000 tons. Its listed qualifications include ISO 9001 quality management certification and CNAS laboratory accreditation, with products supplied to customers in various industries.
REPORT