




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Build Audit-Ready Plastic Tooling Documentation
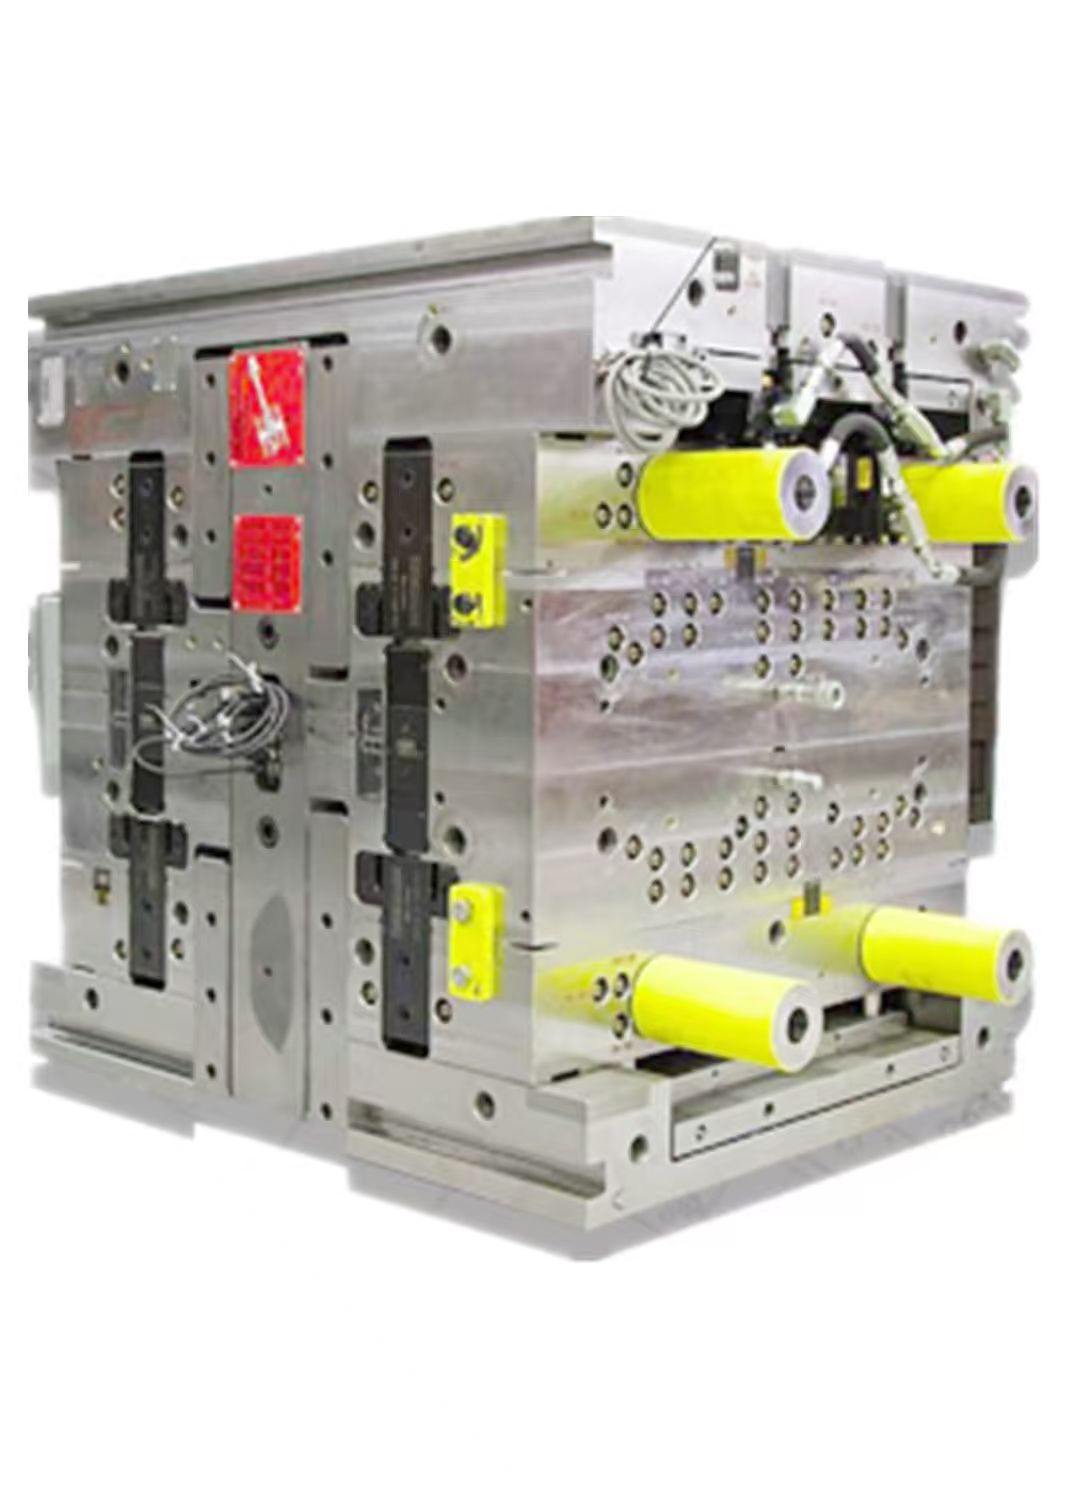
An audit-ready plastic tooling file should provide a clear, traceable record from the approved product requirements through mold design, manufacturing, inspection, delivery, and after-sales support. For Custom Plastic Injection Tooling, the documentation should verify the selected materials, ±0.02 mm precision tolerance, inspection activities, and expected mold life of 50,000–1,000,000 shots.
What an Audit Package Should Demonstrate
Customer and third-party auditors need to confirm that the delivered tooling matches the agreed technical, quality, and commercial requirements. A well-organized file set should therefore combine the mold specification, material certificates, dimensional records, trial reports, sample approval, delivery information, and service commitments.
- Identify the mold base as S50C or P20 and the cavity steel as 718H, 1.2738, or S136.
- Record whether the mold uses a cold-runner or hot-runner system.
- State the required precision tolerance of ±0.02 mm and the anticipated mold life of 50,000–1,000,000 shots.
- Attach mold-trial results, dimensional inspection reports, pre-shipment inspection records, and customer sample approval.
- Include applicable first-article inspection, full-dimension measurement, CMM, surface inspection, and multi-cycle trial records.
- Reference ISO 9001:2015 certification, maintenance instructions, online technical support, and spare-parts availability.
Recommended Documentation Structure
1. Approved Requirements and Tooling Specification
Start with the customer-approved product drawings, mold requirements, revision status, and application. The file should then list the selected mold base, cavity material, runner configuration, dimensional tolerance, expected service life, and agreed delivery schedule. Connecting the tooling to its intended use, such as consumer-electronics housings or home-appliance components, helps auditors assess whether the design and material choices are appropriate.
For Custom Plastic Injection Tooling, the documented options include S50C or P20 mold bases, 718H, 1.2738, or S136 cavity steel, and either cold-runner or hot-runner construction. The specified precision level is ±0.02 mm, while the expected mold-life range is 50,000–1,000,000 shots.
2. Process and Quality Evidence
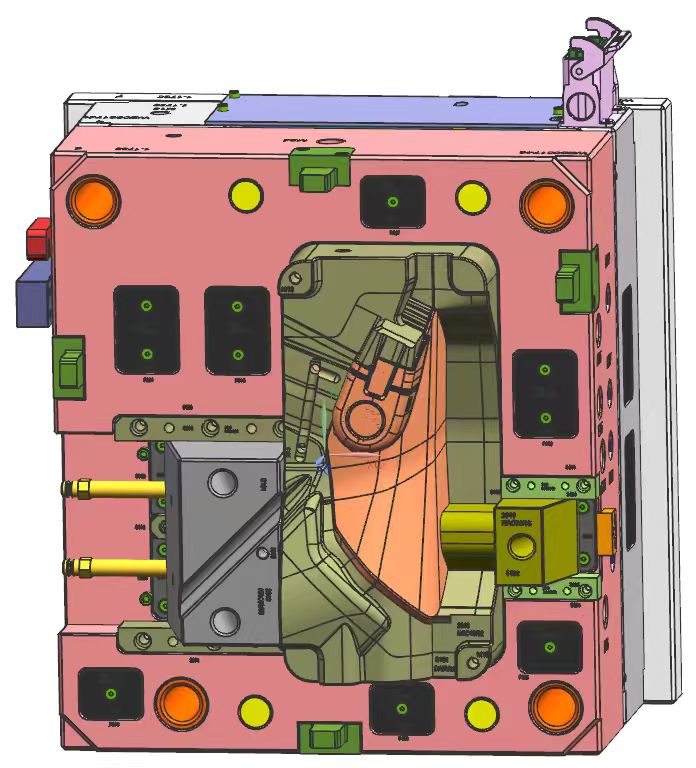
Quality records should follow the tooling process from trial production to final release. Include mold-running or trial-test results, dimensional inspection, surface checks, and the complete pre-shipment inspection. When required by the project, add first-article inspection, full-dimension measurement, CMM reports, multi-cycle mold trials, IQC, IPQC, FQC, and signed sample approval.
Every report should identify the mold or project number, inspection date, responsible personnel, equipment used, acceptance criteria, measured results, and approval status. This makes it easier to trace nonconformities, corrective actions, and the final shipment decision.
3. Commercial and Service Records
The audit file should also clarify the selected business model: OEM custom plastic injection molds, mold making combined with injection molding, high-precision double-shot or overmolding, or mold development followed by plastic injection mass production. Custom Plastic Injection Tooling is listed with a minimum order quantity of one set and a delivery period of 25–40 days.
Include shipping or delivery records, customer communication, sample-release documentation, maintenance guidance, online technical support details, and spare-parts arrangements. These records demonstrate that support continues beyond the initial mold delivery.
Company Credentials and Supporting References
The documentation may reference ISO 9001:2015 certification, certificate number 02825Q12549R0S, covering the design, manufacture, and sale of precision molds and the sale of plastic products. Relevant cooperation examples include electronic housing tooling for an Italian manufacturer, double-shot overmolding tooling for a French product brand, a home-appliance mold for a US brand distributor, and an industrial plastic-part mold for an Australian manufacturer.
Audit Documentation Checklist
| File Section | Recommended Contents |
|---|---|
| Technical specification | Mold base, cavity steel, runner type, tolerance, mold-life target, and application |
| Inspection and validation | Trial results, dimensional inspection, CMM or full-dimension reports, surface checks, and pre-shipment inspection |
| Approval records | First-article documentation, sample confirmation, sign-off, and revision history |
| Commercial information | One-set minimum order quantity, 25–40-day delivery time, and applicable international service scope |
| Support and credentials | ISO 9001:2015 certification, maintenance instructions, technical support, and spare-parts supply |
Frequently Asked Questions
What technical details are essential in a plastic tooling audit file?
List the mold base and cavity steel, runner design, ±0.02 mm tolerance, 50,000–1,000,000-shot service-life range, inspection criteria, trial outcomes, and final inspection status.
Which records are most useful for a third-party audit?
Useful evidence includes mold-trial reports, dimensional and full-dimension inspections, first-article inspection, CMM results, surface inspection, mold-running tests, multi-cycle trials, IQC, IPQC, FQC, and customer sample approval where applicable.
Should company certifications and project references be included?
Yes. Add ISO 9001:2015 certification information, certificate number 02825Q12549R0S, and relevant project references involving electronic housings, double-shot overmolding, home appliances, and industrial plastic parts.
Final Recommendations
A strong plastic tooling audit package is more than a collection of reports. It should form one traceable chain linking customer requirements, material selection, mold construction, dimensional performance, trial validation, sample approval, delivery, and ongoing support. Longterm supports OEM mold production, injection molding, precision double-shot and overmolding, and mold development for mass production. For technical consultation or project support, contact rogerluo@longterm-mold.com.
About Us
Longterm Manufacturing Solutions Limited, also known as Longterm Mold, was established in 2010 and serves customers in the United States, Europe, Australia, and other global markets. The company employs 50 people and provides mold design, tooling, precision machining, mold manufacturing, and plastic parts production. Its R&D team includes five engineers experienced in mold and precision-machining development, UG, SolidWorks, AutoCAD, injection-mold structural design, precision CNC components, sample validation, and process improvement. Longterm holds ISO 9001:2015 certification and has completed projects for customers in several industries.
REPORT