




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Select a Fastener Press Tool for Different Material Thicknesses
Selecting a press tool for fasteners requires more than checking material thickness. The complete material stack, material properties, fastener design, required joining force, and workspace access must all be reviewed. For reliable results, the selected tool and settings should be confirmed through tests using the actual production materials.
Essential Selection Criteria
Start by measuring the combined thickness of every layer in the joint. Then identify the material combination, fastener type, joint geometry, and quality requirements. These factors determine whether the tool can generate a stable and repeatable connection.
- Measure the total material stack rather than evaluating one sheet in isolation.
- Confirm the joining method and fastener specification before choosing equipment.
- Consider material strength, hardness, coating, and access around the joint.
- Use application trials to establish the correct force and process settings.
QUESTOK SPR Riveting Gun Force Range
The QUESTOK SPR riveting gun offers an adjustable output pressure from 1-80 kN. This broad, precisely controllable range allows the process to be adapted to different joining conditions. However, the available product information does not provide a direct chart that matches a particular material thickness to a specific pressure value.
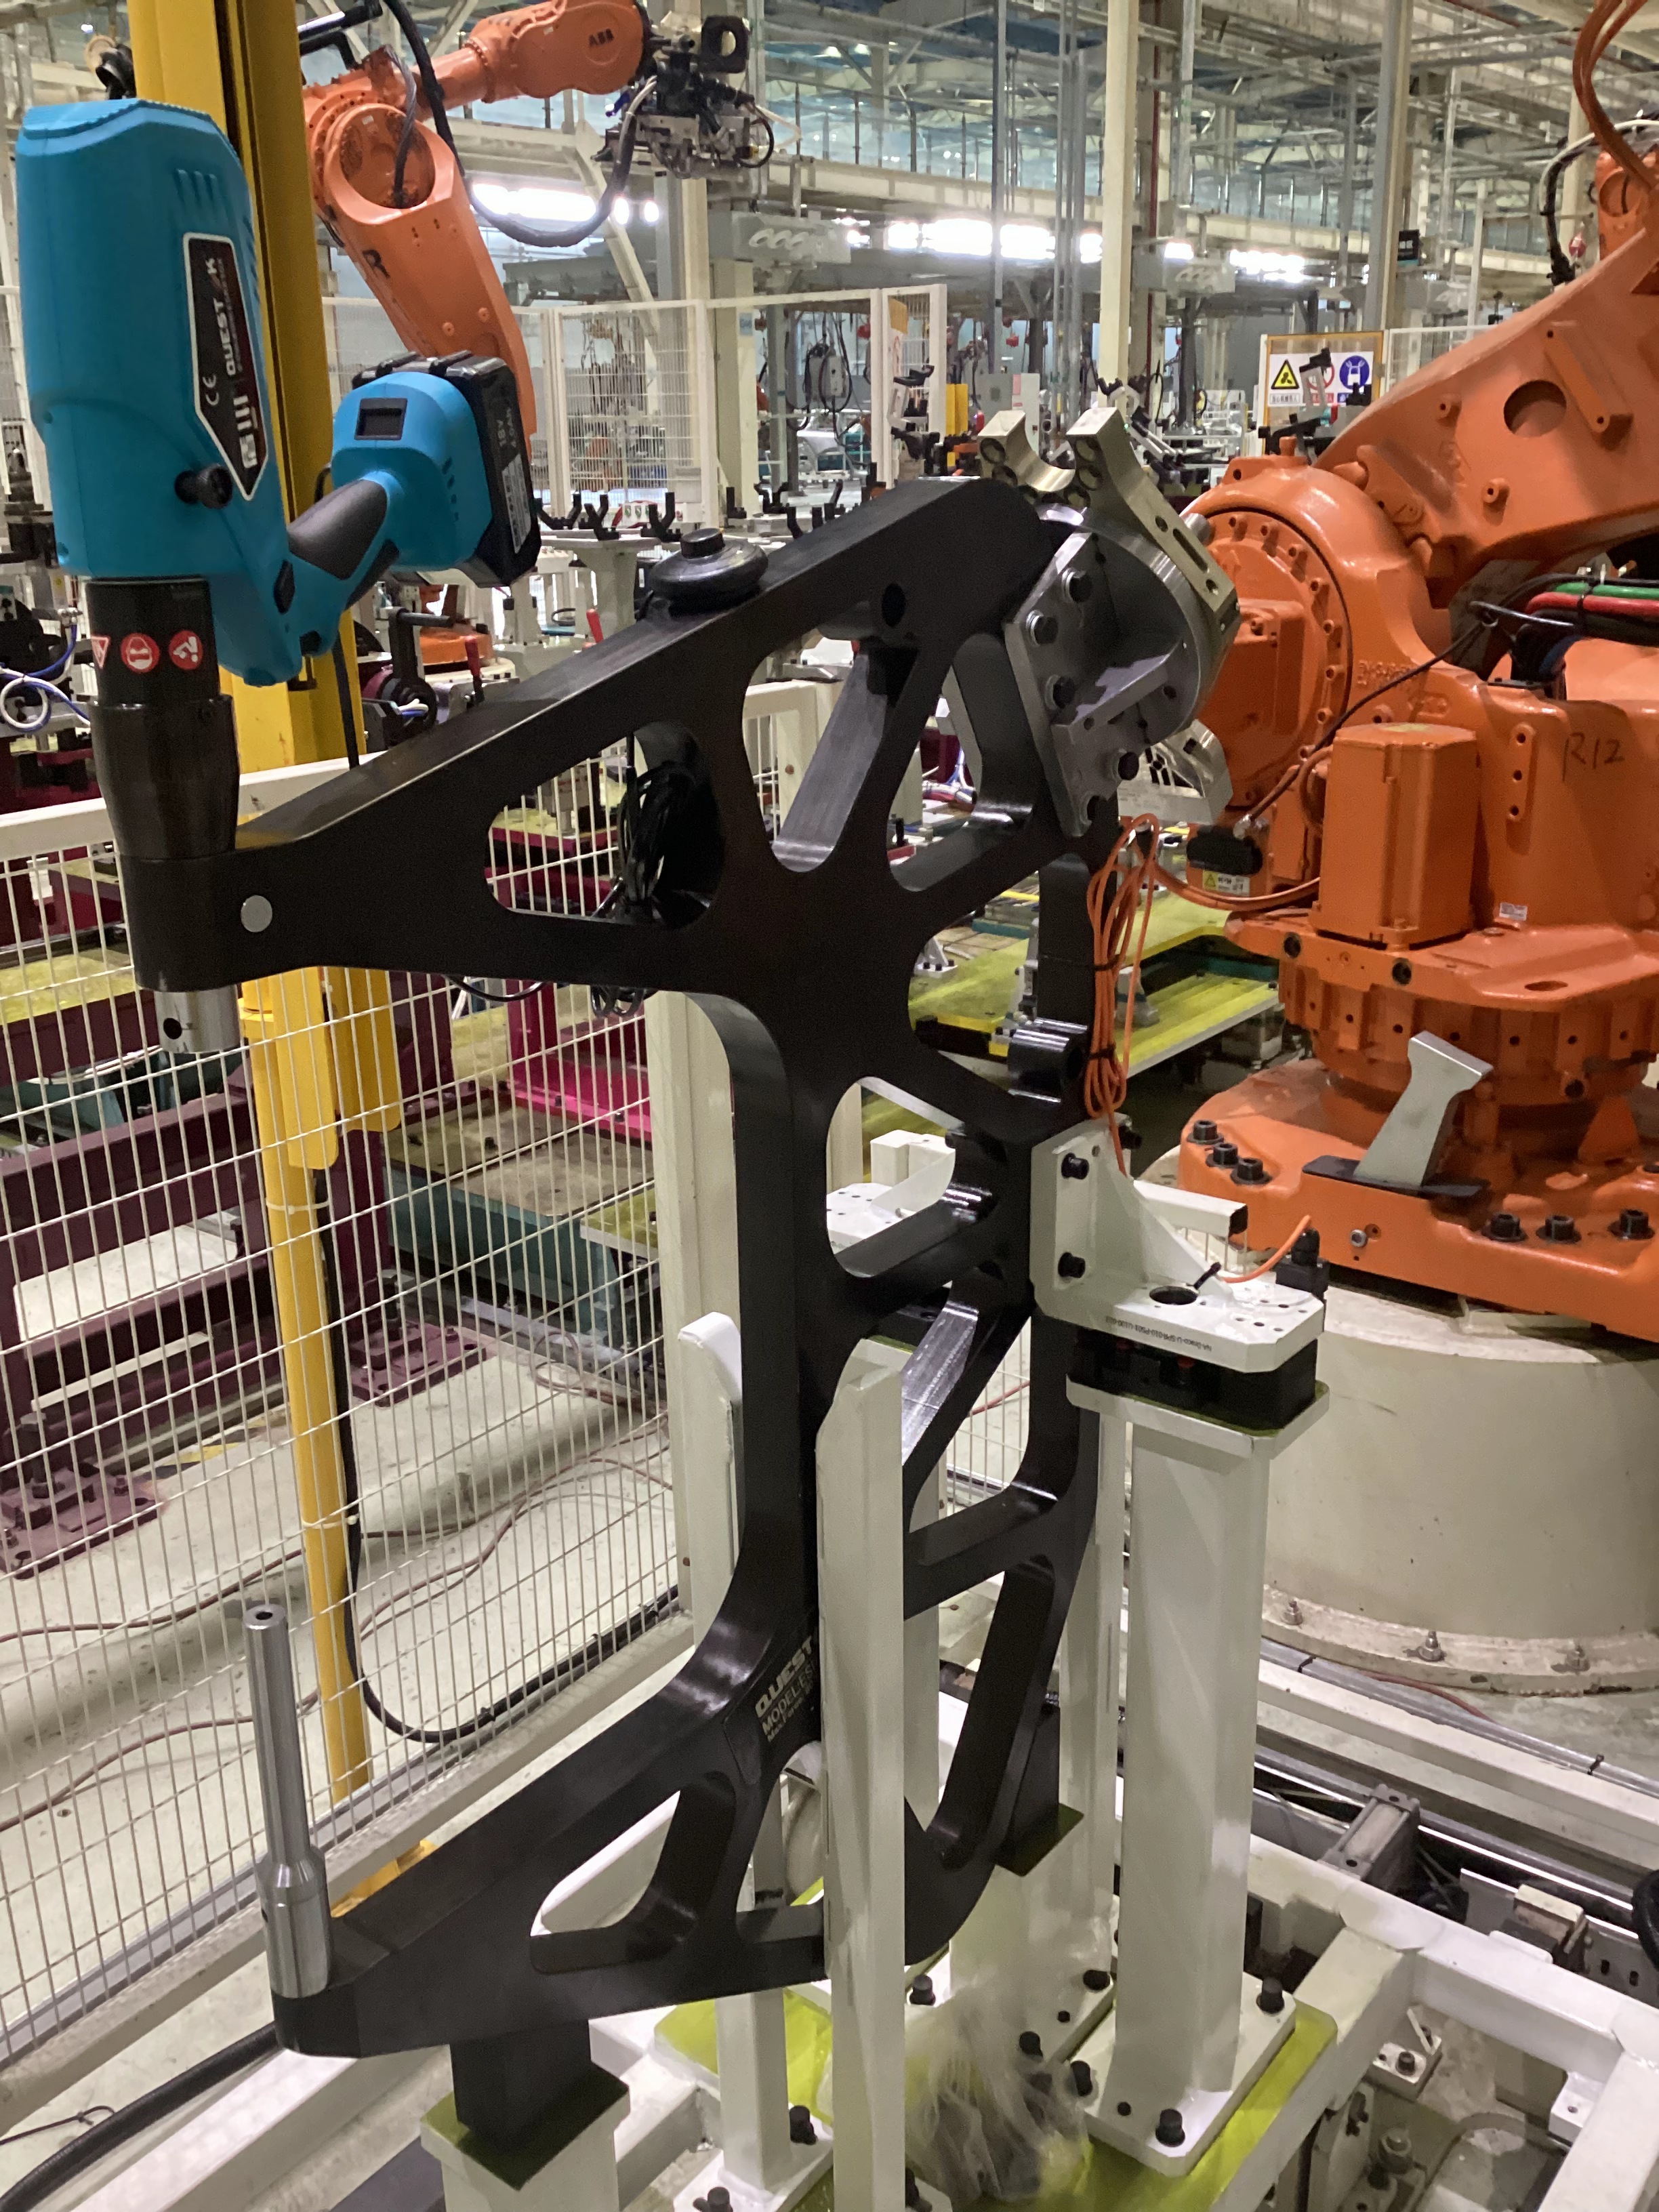
Because thickness alone does not determine the required joining force, the final pressure should be established by testing the intended material stack. The trial should confirm the joint appearance, installation depth, holding performance, and any relevant destructive or metallographic inspection results.
Why Application Testing Matters
A setting that works for one assembly may not be suitable for another, even when the overall thickness appears similar. Differences in aluminum grade, steel strength, coatings, fastener dimensions, die design, and joint location can significantly change the required process force.
A practical validation process includes recording the material stack, identifying the joint position, selecting a tool with a suitable force-control range, and producing trial joints. Inspect the results, adjust the dies or pressure when necessary, and document the approved parameters. Any change in material, fastener, or joint design should trigger a new validation cycle.
Automotive and EV Assembly Applications
QUESTOK documents self-piercing riveting applications for aluminum vehicle bodies. Its application range also includes waterproof nut installation and washer pressing for EV battery trays and water cooling plates. These examples demonstrate why press-tool selection should be based on the complete assembly process, not on sheet thickness as an isolated value.
For complex automotive projects, the company describes testing multiple material combinations, conducting metallographic analysis, modifying dies, and repeating trials before deploying SPR and clinching equipment. This type of engineering verification is especially important when joining high-strength materials or safety-critical components.

Selection Data and Validation Actions
| Selection item | Recommended approach |
|---|---|
| Total material thickness | Measure the complete stack; the available product data does not specify a universal thickness limit. |
| Available joining force | The QUESTOK SPR riveting gun provides 1-80 kN of precisely adjustable output pressure. |
| Material combination | Test the actual materials, coatings, fastener, die, and joint configuration. |
| Typical applications | Documented areas include automotive bodies, EV battery trays, and water cooling plates. |
| Quality confirmation | Use visual, dimensional, performance, or metallographic inspection as required by the application. |
| Ordering and delivery | MOQ is 1 set. Standard products below 50 sets are listed with delivery in 3 days against payment, while customized solutions require 15 days. |
Frequently Asked Questions
Can material thickness alone determine the correct press tool?
No. Total stack thickness is an important starting point, but material properties, fastener geometry, joint access, required quality, and the joining method must also be considered. Since no thickness-to-pressure chart is supplied, application testing is required.
What pressure range is available on the QUESTOK SPR riveting gun?
The listed output pressure range is 1-80 kN, with precise adjustment. The correct pressure for a specific assembly is not predefined and should be developed through trials on the production material combination.
Can the system be used for EV battery assemblies?
QUESTOK identifies SPR riveting, waterproof nut installation, and washer pressing for EV battery trays and water cooling plates as application areas. Final suitability depends on the design, materials, fasteners, and validation results.
Conclusion
To match a fastener press tool to material thickness, measure the entire stack and evaluate the joining method, material combination, fastener, die, and access conditions. The QUESTOK SPR riveting gun provides a 1-80 kN precisely adjustable output range, but the supplied information does not define a universal thickness limit. Confirm the final tool and pressure setting through application tests on the actual assembly.
Questok supports ODM and OBM cooperation, with an MOQ of 1 set, full inspection, and a stated global after-sales response within 24 hours. For technical guidance or a customized fastening solution, contact jane@questok.com.
About Us
PHOTON TECHNOLOGY KUNSHAN CO.,LTD, operating under the Questok brand, develops equipment for fastening, joining, and industrial assembly. Founded in 2011, the company focuses on industrial design, hydraulic systems, electrical controls, battery-powered tools, fastening-process development, prototype testing, and reliability verification. Its portfolio includes SPR riveting systems, self-piercing riveting guns, clinching equipment, fasteners pressing tools, and integrated joining solutions. The company lists CE and MSDS certifications and serves customers across several manufacturing industries.
REPORT