




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Test Insulated Mailer Samples Before Cold-Shipping Production
Before approving mass production, an insulated mailer sample should be evaluated for temperature retention, construction quality, sealing reliability, dimensional accuracy, closure function, food-contact safety, moisture control, print quality, and handling strength. For cold-shipping applications, confirm that the aluminium foil laminate, closed-cell EPE foam, food-grade PE sealant, zipper or heat-sealed opening, and moulded handle all match the approved specification and shipping conditions.
Pre-Production Testing Priorities
A reliable approval process begins by testing the sample as it will be used in the field. Load it with the intended product and coolant, close it using the selected method, and expose it to delivery conditions that reflect the planned cold-chain route. The results should show whether the mailer provides adequate thermal protection without depending on unverified assumptions about its insulation structure.
- Confirm that the specified foil laminate and insulation core support the required holding time with the planned gel-pack layout and shipment contents.
- Examine the flat pouch, three-side seals, internal contact layer, closure, and handle for visible defects and consistent workmanship.
- Check the usable capacity, loading process, closure operation, carrying performance, stacking behaviour, and compatibility with an outer courier bag when required.
- For grocery, pharmaceutical, and other last-mile cold-chain uses, review gel-pack sleeve placement, condensation containment, and space for labels or temperature indicators.
- For e-commerce fulfilment, compare foil, zipper, bubble-lined, and kraft-paper outer constructions against the protection, presentation, and logistics needs of the shipment.
Construction and Material Verification
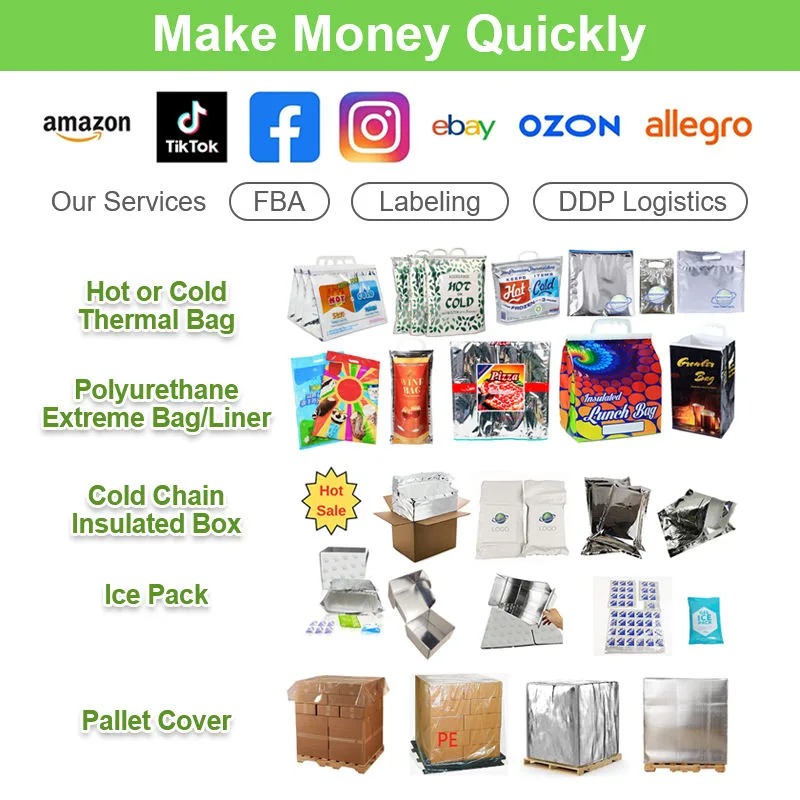
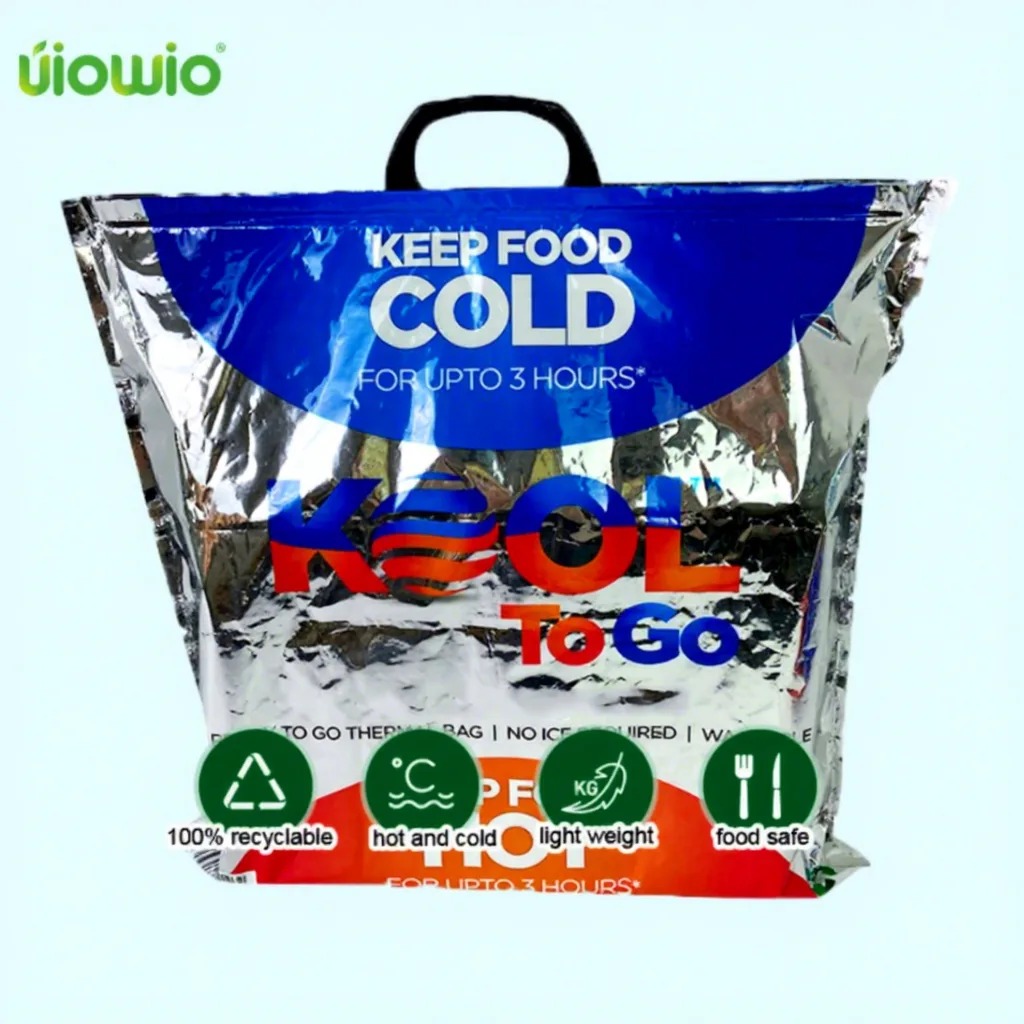
Compare the physical sample with the approved drawing, specification, and artwork before authorizing production. The referenced design is a flat pouch with three sealed sides and no gusset. Its exterior consists of an aluminium foil laminate with full-colour printing, while the insulation layer is closed-cell EPE foam specified at 2-5 mm. Because an air-bubble core can also be supplied on request, the sample documentation must identify the exact structure being evaluated.
Seals and Opening Performance
Inspect the entire heat-sealed perimeter for uninterrupted bonding, smooth edges, wrinkles, channels, incomplete fusion, and possible leakage paths. When a zipper is specified, cycle it repeatedly and pay particular attention to the sealed ends. When the mouth is heat sealed, verify that it closes evenly and can be loaded efficiently without damaging the seal or the contents.
The food-grade PE sealant forms the product-contact layer. Confirm that the correct material is present and that the inner face is clean, smooth, intact, and free from delamination. The foil laminate should also be checked for pinholes, scratches, peeling, exposed foam, and weak bonding that could reduce moisture or thermal-barrier performance during transport.
Dimensions, Capacity, and Handle Strength
Measure the finished pouch against the approved size, which may range from 30 x 18 cm to 49 x 51 cm depending on the selected format. Measure the usable interior after sealing rather than relying only on the flat dimensions. The intended food container, parcel, and gel pack should fit without excessive compression or unnecessary empty space.
Load the pouch and lift it using the moulded plastic grip. Examine the welded handle connection through the top seal for distortion, tearing, separation, or progressive damage during repeated short-distance handling. Also confirm that the handle location remains comfortable and does not interfere with the closure or the loading sequence.
Cold-Chain and Appearance Tests
Record the starting temperature, product or test load, coolant type and position, ambient conditions, package orientation, and total test duration. For designs intended for grocery or pharmacy delivery, inspect the dedicated gel-pack sleeve to ensure that it is correctly positioned, keeps coolant separate from the product, and provides practical protection against condensation. Confirm whether there is sufficient room for batch identification, temperature-monitoring devices, or handling labels.
Visual inspection should include print registration, colour uniformity, logo placement, foil finish, temperature bands, and the accuracy of labelling areas. Ecopack reports that new designs are approved using a physical bag, with Pantone-matched samples generally completed within 3 to 5 working days. The approval sample should therefore be treated as the reference for production appearance.
Quality control is organized through incoming-material, in-process, and pre-shipment inspection under the ISO 9001:2015 system. Finished mailers are checked through AQL sampling for appearance, dimensions, print registration, seal strength, and lamination bond. FSC Chain of Custody certification applies to specified paper and packaging products and should not be interpreted as a substitute for confirming the foil insulated mailer materials.
Testing Checklist and Product Comparison
| Evaluation Area | Approval Question | Applicable Product Information |
|---|---|---|
| Thermal retention | Does the selected structure maintain the required protection with the intended coolant and delivery duration? | Aluminium foil laminate with closed-cell EPE foam; air-bubble core available on request |
| Seal and closure | Are all seals continuous, clean, leak-resistant, and repeatable during use? | Three-side seal with either a zipper or heat-sealed mouth |
| Food-contact layer | Does the inner surface use the approved material and remain clean and undamaged? | Food-grade PE sealant |
| Fit and carrying | Does the pouch meet dimensional tolerances and safely hold, close, and carry the planned load? | Flat pouch sizes from 30 x 18 to 49 x 51 cm with moulded plastic grip |
| Printing and identification | Are colour, registration, logo position, temperature markings, and label zones correct? | Full-colour printing with customizable structure, size, core, colour, and logo |
| Production consistency | Can the approved sample be reproduced consistently and supported by inspection records? | Sampling in 3 to 5 working days; production in 15 to 25 days after artwork approval |
Frequently Asked Questions
Which insulation materials must be confirmed in the sample?
The sample should contain the approved aluminium foil laminate, closed-cell EPE foam core, and food-grade PE sealant. If the project uses an air-bubble core or another alternative, that construction should be stated clearly on the sample record so that test results are not compared with the wrong specification.
How can the zipper, heat seal, and handle be evaluated?
Operate the zipper through multiple opening and closing cycles and inspect both ends and the surrounding seal. For a heat-sealed mouth, check bonding uniformity and resistance to normal loading. Lift a filled pouch by its moulded plastic handle and inspect the welded connection for separation, stretching, or distortion.
What should be done when delivered goods do not match the approved sample?
Record the affected units and photograph the carton label, product details, and visible defects. Ecopack states that it traces the batch through its production records, verifies the claim, and agrees on replacement or credit when appropriate. The stated response time for each claim is within two working days.
Production Approval Recommendations
Mass production should proceed only after the sample passes thermal, material, sealing, closure, dimensional, handle, condensation, print, and labelling checks. The evaluation should use the same product load, coolant arrangement, and handling sequence expected after launch. This is especially important for cold-chain programs, where thermal results depend on the complete package rather than the mailer alone.
A documented cold-chain project for a US distributor involved an annual volume of 10 million insulated mailers. The reported objective was to reduce heat transfer while saving storage and shipping space compared with rigid foam packaging. This example supports reviewing both temperature performance and carton efficiency before final approval. Custom orders commonly begin at approximately 5,000 to 10,000 pieces depending on size and structure, while stock formats may be shipped from available inventory. Standard production is scheduled for 15 to 25 days after artwork approval. For technical support, contact manager@ecoppack.com.
About the Manufacturer
Huizhou Ecopack Packaging Products Co., Ltd. is a flexible packaging manufacturer based in Guangdong, China. Established in 2011, the company produces custom composite pouches and bags, including insulated mailers, thermal packaging, coffee packaging, pet food packaging, spout pouches, kraft and compostable formats, and ESD bags. Its 10,000+ sqm facility integrates R&D, printing, lamination, bag making, and inspection. The company holds ISO 9001:2015 Quality Management System certification and FSC Chain of Custody certification for applicable products.
REPORT