




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Verify an Electrostatic Flocking Fabric Sample Before Mass Production
Approving an electrostatic flocking fabric sample requires more than a visual color comparison. The approved sample should be used as the benchmark for the production batch, with checks covering fabric construction, color, pile height, density, texture, adhesion, abrasion resistance, dimensions, chemical safety, and traceability. Instrument testing and production records should support the final approval decision.
Sample Approval Checklist
- Confirm that the production batch uses the same base fabric, flock fiber, pile structure, backing, finishing method, and color reference as the approved sample.
- Compare appearance, pile direction, pile height, density, gloss, hand feel, width, roll length, and packaging construction.
- Use spectrophotometer readings, dimensional inspection, adhesion tests, abrasion testing, and visual checks to verify the production material.
- For jewelry packaging, include reactive sulfur, pH, chloride, volatile acid, and silver coupon accelerated corrosion testing.
- Collect batch records, compliance documents, laboratory reports, and pre-shipment inspection results before releasing the order.
1. Confirm the Material Identity and Construction
The approved sample is the physical definition of the product that should be delivered. Begin by checking whether the mass-production fabric has the same substrate, flocking fiber, pile length, color standard, adhesive system, and post-treatment process. A change from spunlace to knitted backing, for example, may affect elasticity, softness, dimensional stability, luster, and bonding performance even if the surface color remains close.
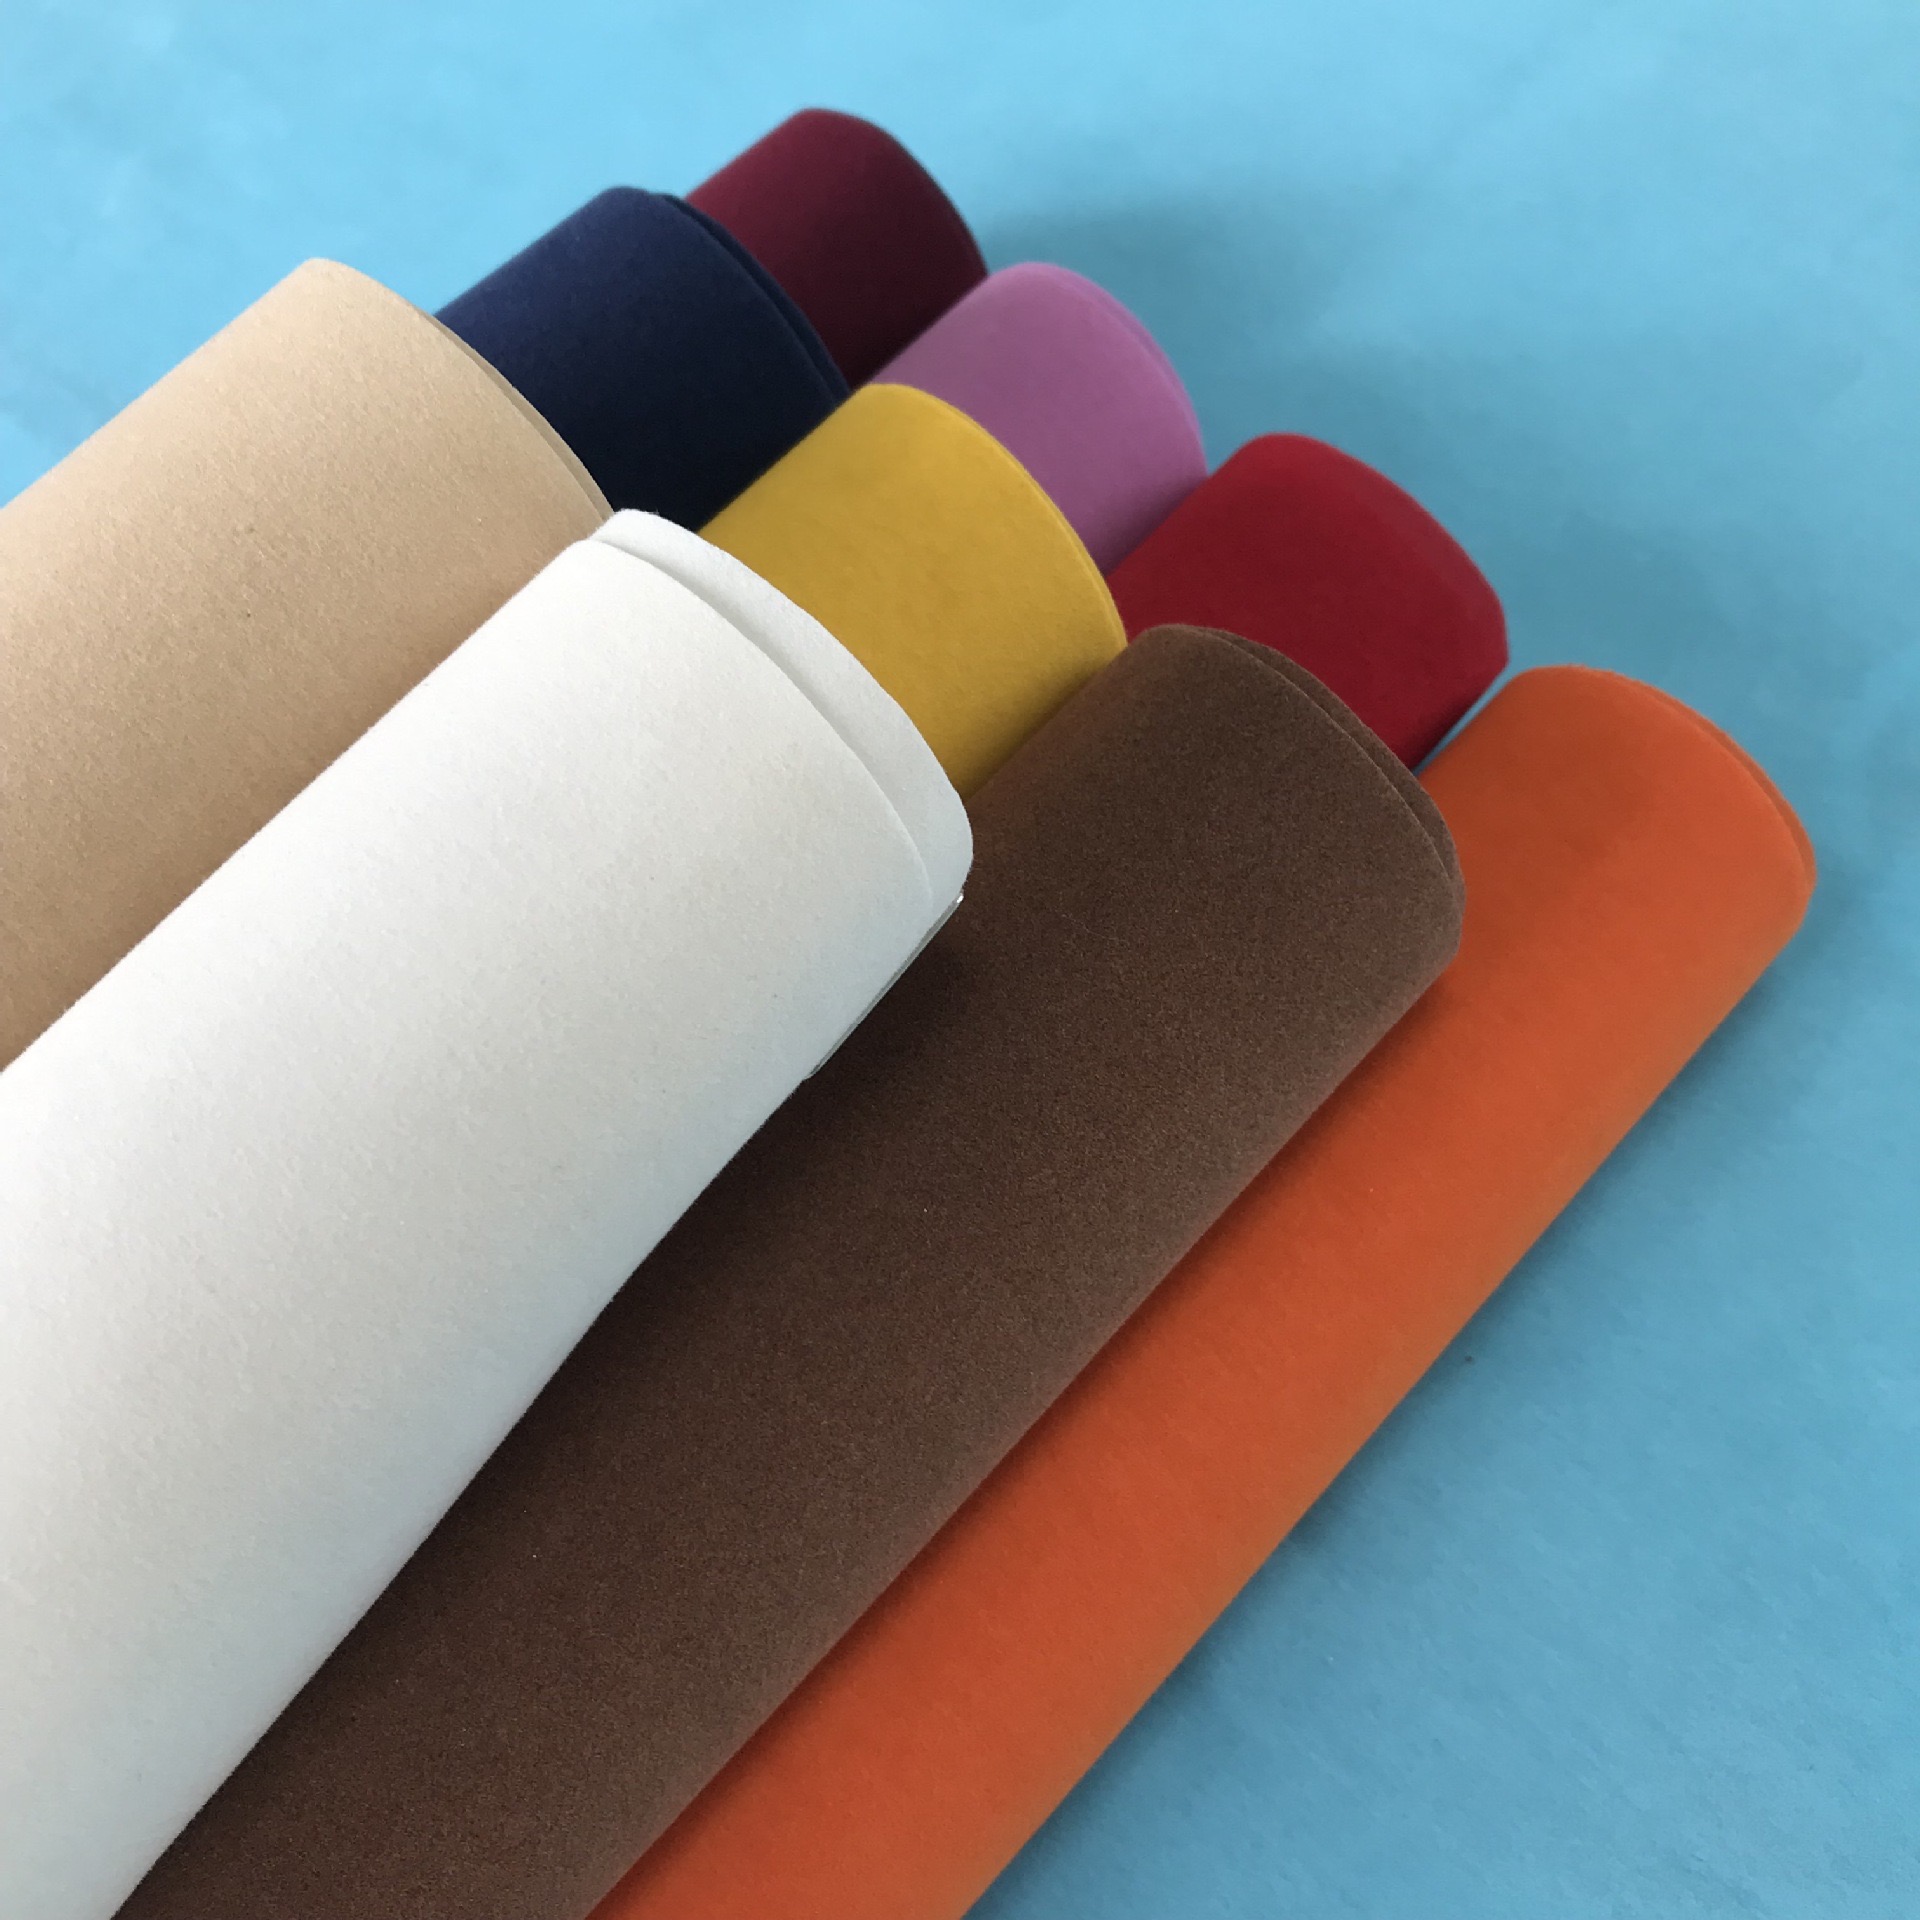
For Long Pile Velvet, the specification generally includes a pile height above 1 mm, a pronounced three-dimensional appearance, saturated color, and a soft, fluffy handle. Depending on the order, the backing may be spunlace, cotton-rayon, or knitted fabric. The reported standard width is 58 inches, with typical roll packaging of 50 to 100 yards. These details should be written into the approved sample specification rather than left to visual interpretation.
2. Compare Color and Surface Appearance
Color comparison should be performed under controlled lighting and against the agreed Pantone reference. A side-by-side visual review is useful, but it should be supported by spectrophotometer data. Mingqian Flocking reports measuring color variation during production at intervals of every 100 yards. The stated target is a Pantone Delta E of no more than 2.0 for standard orders and no more than 0.5 for custom orders, with batch color deviation controlled to no more than 3 percent.
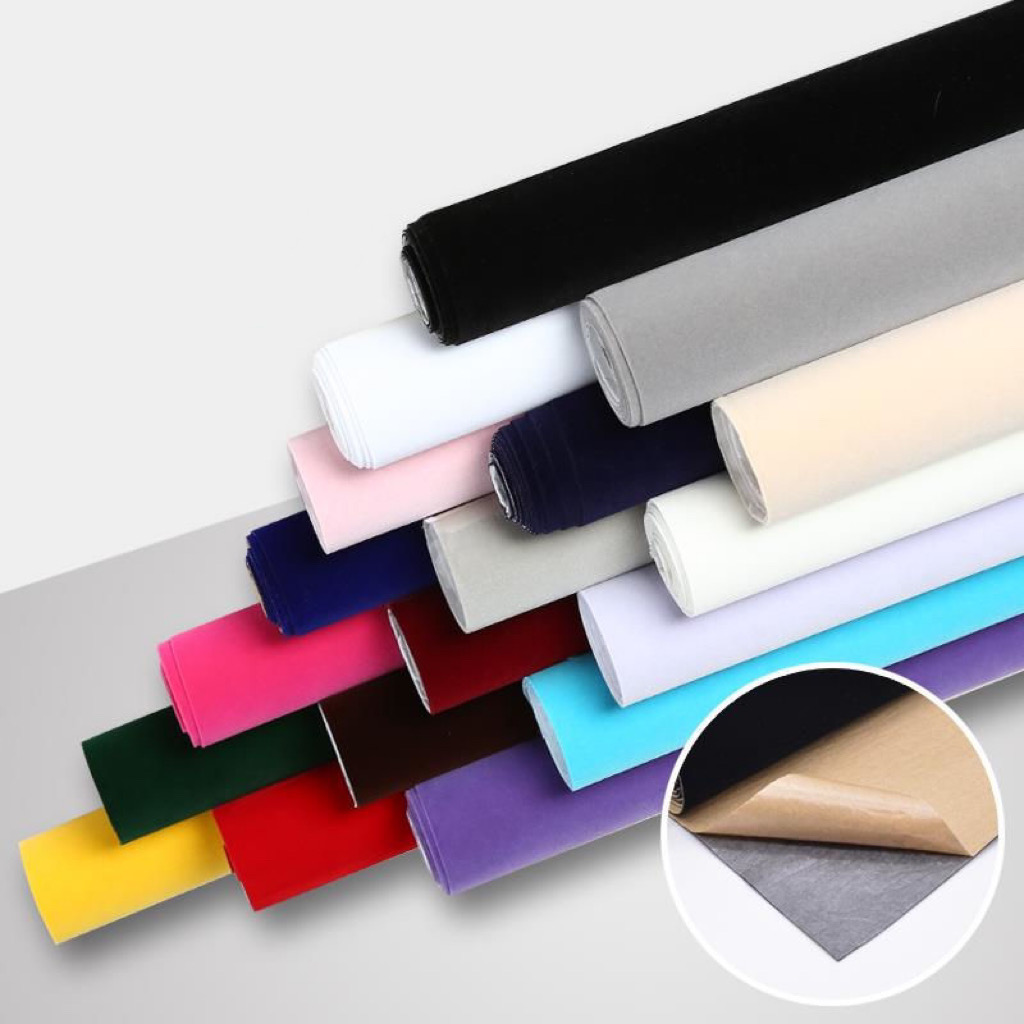
Inspect the start, center, and end of the production roll because surface variation may develop along the manufacturing length. Compare pile direction, density, height, gloss, texture, and softness with the approved sample. Look specifically for exposed backing, thin or missing flock, uneven pile orientation, adhesive bleed-through, streaks, crushed zones, shade variation, and other visible defects. The production material should preserve the sample's three-dimensional effect and consistent hand feel.
3. Test Pile Adhesion and Durability
A fabric can look identical to the sample and still fail during converting or use if the flock fibers are not securely bonded. Use the 3M tape 10-cycle peel method to assess adhesion and inspect the tape and fabric for fiber loss. Under the stated FAMA requirement, no fiber loss is acceptable. For self-adhesive products, the peel strength target is at least 2 newtons per 25 millimeters.
Color fastness should also follow the intended application. The reported requirement for deep shades is Grade 4 under both wet and dry testing, while light exposure fastness should reach Grade 6 or higher. Abrasion resistance must be selected according to the product's use. Standard materials may be tested to 500 cycles, whereas functional products may require up to 100,000 cycles. The applicable specification should clearly state that no shedding is permitted at the approved test level.
4. Verify Dimensions and Processing Stability
Measure the usable width, roll length, cutting accuracy, and finished construction stability. Compare the sample and production batch after any secondary process included in the order, such as hot pressing, silk-screen printing, gold stamping, laminating, or die cutting. These processes can change the appearance, thickness, adhesion, and dimensional behavior of the flocking material.
For customized shapes, Mingqian Flocking reports a precision die-cutting tolerance of plus or minus 0.1 millimeters. The actual tolerance should nevertheless be confirmed against the buyer's drawing and application requirements. Record measurements from several production locations rather than relying on a single reading.
5. Add Chemical and Corrosion Checks for Jewelry Packaging
When the fabric is used inside jewelry boxes, trays, or watch packaging, appearance and mechanical performance are not sufficient. The production material should be tested for substances that may tarnish or discolor metal components. The reported controls include reactive sulfur below 5 parts per million and an aqueous extract pH between 5.5 and 7.5. Chloride and volatile acid levels should also meet the agreed internal or customer specification.
A silver coupon accelerated corrosion test should be performed for every applicable batch. Acceptance requires no blackening, spotting, oxidation, or other discoloration on the silver coupon. The compliance report must correspond to the actual fabric construction and production batch, not to a different substrate or an earlier sample.
6. Match Compliance Documents to the Delivered Fabric
Before approval, request the relevant chemical and environmental documentation. The supplied product information reports internal limits of no more than 75 parts per million for formaldehyde and no more than 30 parts per million for azo dyes. Applicable flocking fabrics made with recycled polyester or nylon may also be supported by Global Recycled Standard certification.
Mingqian Flocking reports ISO 9001:2015 certification. Its SGS REACH documentation covers 253 Substances of Very High Concern plus one potential SVHC, while its RoHS 2.0 report addresses the ten restricted substances listed in the supplied product information. Buyers should verify the report date, material description, test scope, and batch relationship before treating a document as evidence of production compliance.
7. Review Traceability and Inspection Records
Production traceability connects the approved sample with the rolls eventually shipped. A complete record should include the sample code, confirmed construction, Pantone reference, production batch number, raw-material information, inspection results, laboratory reports, and pre-shipment approval.
Mingqian Flocking describes a four-stage quality process covering base-fabric pretreatment, in-house dyeing, adhesive application, electrostatic flocking, drying and curing, post-finishing, and final inspection. Its quality information is digitally archived by batch number, allowing a finished roll to be traced back to its manufacturing records and raw materials.
Sample-to-Production Verification Table
| Inspection Area | How to Compare the Sample and Batch | Reported Control or Target |
|---|---|---|
| Material construction | Check substrate, flock fiber, pile type, backing, adhesive, finishing, width, and roll configuration. | Long Pile Velvet uses a pile height above 1 mm; reported width is 58 inches. |
| Color | Review under consistent lighting and measure against the approved Pantone reference with a spectrophotometer. | Delta E no more than 2.0 for standard orders and no more than 0.5 for custom orders. |
| Pile and texture | Compare pile direction, height, density, softness, luster, three-dimensional effect, and exposed backing. | Reported pile-density control reaches 0.01 millimeter precision. |
| Adhesion | Perform the 3M tape 10-cycle peel test and check for loose or missing fibers. | No fiber loss is required under the FAMA test method; self-adhesive products target at least 2 N/25 mm. |
| Color fastness | Test wet and dry fastness for deep shades and light exposure fastness as specified. | Grade 4 for deep-color wet and dry fastness; Grade 6 or higher for light exposure. |
| Abrasion | Apply the test level associated with the intended end use and confirm that shedding does not occur. | 500 cycles for standard products up to 100,000 cycles for functional products. |
| Dimensions | Measure width, roll length, die-cut shape, and stability after secondary processing. | Customized die-cutting tolerance reported at plus or minus 0.1 millimeters. |
| Chemical safety | Check the material construction, compliance report, and batch test results against the order specification. | Formaldehyde no more than 75 ppm; azo dyes no more than 30 ppm; jewelry-grade reactive sulfur below 5 ppm. |
| Traceability | Record the approved sample number, specifications, batch number, test results, and shipment inspection. | Digital records are archived by production batch for backward traceability. |
Practical Examples of Application Requirements
Different end uses require different acceptance levels. An anonymized luxury perfume packaging program used black nylon flocking with a Pantone Delta E of no more than 0.5 and abrasion performance of 100,000 cycles without shedding. An anonymized jewelry packaging program used spunlace-based medium-pile flocking, with deep-color fastness of Grade 4 or higher and light exposure fastness of Grade 6 or higher.
These examples demonstrate why a sample should not be approved on appearance alone. The buyer should define the performance level according to the finished product, then require the same test method and acceptance criteria for mass production.
Frequently Asked Questions
What should be included in a flocking fabric sample approval?
Include the substrate, flock type, pile height and density, color, hand feel, gloss, surface texture, width, roll length, adhesion, abrasion resistance, color fastness, dimensional tolerance, and relevant chemical requirements. The same checklist must be applied to the production batch.
What is the most reliable way to confirm color consistency?
Use the identical Pantone reference, controlled lighting, and spectrophotometer readings. Mingqian Flocking reports checking color difference every 100 yards, with Delta E targets of no more than 2.0 for standard orders and no more than 0.5 for custom orders.
Which records should be obtained before mass-production approval?
Request the approved sample specification, production batch number, color readings, pile and dimensional inspection data, adhesion and abrasion results, chemical reports, applicable silver coupon corrosion results, and the final pre-shipment inspection record.
Final Recommendation
Mass production should be accepted only when the delivered fabric matches the approved sample in construction, color, pile appearance, dimensions, adhesion, durability, and compliance performance. For OEM and ODM programs, the supplied product information lists a minimum order quantity of 1,000 yards and a delivery period of 14 days. These commercial details, along with the technical specification and inspection plan, should be confirmed before production begins.
Mingqian Flocking combines ISO 9001:2015 quality management, GRS certification for applicable recycled-fiber fabrics, batch traceability, and a four-stage inspection process. For technical support or a customized flocking solution, contact 005@mingqianflocking.com.
About Mingqian Flocking
Guangdong Shunde Mingqian Flocking Co., Ltd., operating under the Mingqian brand, is a flocking fabric manufacturer based in Foshan, Guangdong, China. Established in 2008, the company focuses on the research, development, production, and sales of flocking fabrics. Its self-owned facility covers more than 12,000 square meters, with five flocking production lines and a reported capacity exceeding 3,000,000 yards per month. The company holds ISO 9001:2015 and Global Recycled Standard certification and supplies flocking materials for packaging and other industrial applications.
REPORT