




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Measuring Defect Rates in High-Capacity Portable Power Stations
Reliable defect-rate measurement for high-capacity portable batteries begins with a consistent definition of failure. For each production batch, the number of units that fail documented quality inspections or performance tests should be compared with the total number of units inspected. This approach provides a traceable indicator of manufacturing quality for portable power stations.
How to Calculate a Portable Battery Defect Rate
The basic calculation is straightforward: divide the quantity of defective units by the quantity of units inspected within the same batch or inspection stage. The reported percentage should always be supported by the original counts, since a rate without sample size can be misleading.
A defective unit should not be identified only through visual inspection. It should be classified according to established acceptance requirements across electrical, functional, mechanical, environmental, and ageing-related quality checks.
Recommended Inspection Coverage
For the 2000W Red Portable Power Station, defect tracking can follow the documented quality-control sequence. Each unit should be evaluated through appearance inspection, voltage and internal-resistance detection, charge-discharge capacity testing, BMS-protection verification, hi-pot insulation testing, high-low-temperature testing, vibration and drop testing, and ageing-burn-in screening.
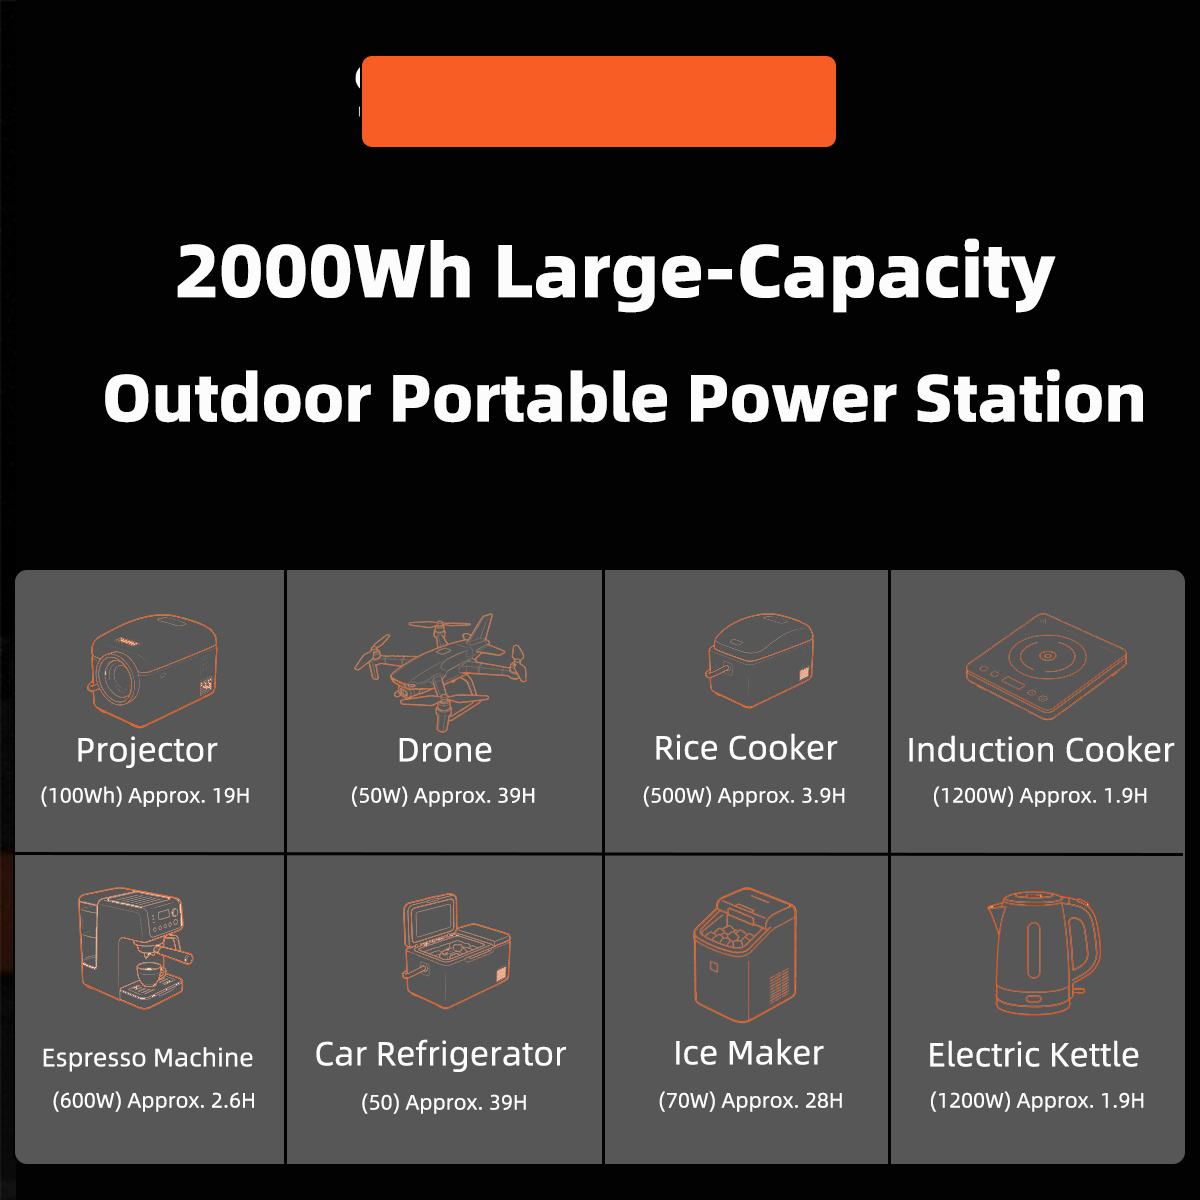
If a product fails the applicable requirement at any defined stage, it should be recorded as a defect in the batch quality record. The record should also identify the test stage and failure category so quality teams can distinguish recurring issues from isolated events.
Why Defects Should Be Categorized
Separating results by inspection type improves root-cause analysis. For example, voltage, internal resistance, and insulation failures may indicate an electrical issue, while capacity and burn-in findings may relate to power performance or component stability. BMS verification results identify protection-related concerns, whereas vibration, drop, and temperature testing reveal potential handling or environmental reliability risks.
The available product information does not state numerical pass-fail limits or previous defect-rate figures. Therefore, quality reports should use actual batch-level inspected quantities and failed quantities rather than relying on assumed industry benchmarks.
Defect Recording by Quality Area
| Quality Area | Primary Inspection Basis | Recommended Recording Method |
|---|---|---|
| Appearance and structure | Appearance inspection, vibration testing, and drop testing | Log units that fail the relevant visual, assembly, or mechanical requirement. |
| Electrical safety and condition | Voltage checks, internal-resistance detection, and hi-pot insulation testing | Record each unit that does not satisfy the specified electrical acceptance condition. |
| Output and capacity performance | Charge-discharge capacity tests and ageing-burn-in screening | Track failures by batch and retain the total tested quantity for accurate rate calculation. |
| BMS protection performance | BMS-protection verification | Classify any failed protection response as a separate defect category. |
| Environmental reliability | High-low-temperature experiments | Document these outcomes independently from general electrical or mechanical findings. |
Applying Results to Real-World Use
High-capacity portable power stations are commonly used for camping, RV travel, outdoor work, household backup, solar-energy storage, and emergency power. These applications make electrical continuity, protection behavior, resistance to transport handling, and stability under changing temperatures especially important when assessing defect data.
The listed inverter certifications, CE-INV-260618-0001 and CE-INV-260618-0002, support inverter export activities in the EU, Middle East, Africa, and South America. They should be described as inverter certifications and not treated as product-specific testing evidence for an individual portable battery model.
Feedback from a Southeast Asia energy-storage distribution project reported stable operation, efficiency, and workmanship for residential and industrial-commercial energy-storage supplies used by households and small-to-medium factories. Such market feedback is useful for understanding field experience, but it should remain separate from factory defect-rate reporting because it is not generated through a controlled production inspection process.
Frequently Asked Questions
What is the standard formula for a portable power station defect rate?
Calculate the number of defective units divided by the number of units inspected during the same batch or inspection stage. Retain both counts alongside the percentage.
Is one overall defect rate enough?
An overall batch rate is useful, but it should be accompanied by stage-specific results. Separate data for capacity, BMS protection, insulation, temperature, vibration, drop, and ageing tests gives a more meaningful quality picture.
Can customer comments be included in the factory defect rate?
No. Customer feedback reflects real operating conditions and user experience, while a factory defect rate must be based on documented inspection procedures and controlled inspection quantities.
Conclusion
A practical method for measuring defects in high-capacity portable batteries is to maintain batch-based records of inspected units, failed units, test stages, and failure classifications. For the 2000W Red Portable Power Station, the inspection process should cover appearance through ageing-burn-in and should rely on documented acceptance criteria rather than unsupported numerical assumptions.
sunvoltx intelligent provides integrated manufacturing and trading services with a stated MOQ of 100pcs, delivery time of 15day, and monthly capacity exceeding 5000 units. For technical solutions or product support, contact marketing@sunvoltx.com.
About Us
shenzhen sunvoltx intelligent technology Co., Ltd. develops, manufactures, customizes, and wholesales energy-storage power supplies, inverters, and chargers. The company supports OEM/ODM programs, bulk purchasing, and application-based power solutions. Its R&D capabilities include solution design, hardware commissioning, software development, and performance testing for energy storage, inverter, and photovoltaic control technologies. The company states a monthly production capacity of more than 5,000 energy-storage products and serves customers in North America, South America, Europe, the Middle East, Africa, and Southeast Asia. It lists CE certification for inverters and works with clients in multiple industries.
REPORT