




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
The Eco-Friendly Revolution: How Water-Based Inks Are Redefining Custom DTG Apparel Manufacturing
The Sustainable Shift in Direct-to-Garment Printing
The modern streetwear landscape is undergoing a major transformation driven by sustainable direct-to-garment (DTG) innovation. By substituting hazardous PVC plastisols, heavy metal additives, and volatile solvents with eco-conscious water-based pigment formulations, apparel manufacturers can now drastically lower their ecological footprint. Beyond environmental compliance, this printing technology yields superior fabric breathability and an exceptionally soft hand-feel, making it ideal for premium heavyweight cotton garments.
Understanding the Technology: Mechanism and Fiber Bonding
Unlike conventional screen printing methods that lay down a stiff synthetic layer on top of textiles, water-based DTG printing relies on specialized aqueous pigment dispersions suspended in water-compatible liquid carriers. During application, the ink penetrates deeply into pre-treated natural fibers. Heat curing subsequently evaporates the water base, permanently locking non-toxic color pigments into individual yarn filaments.
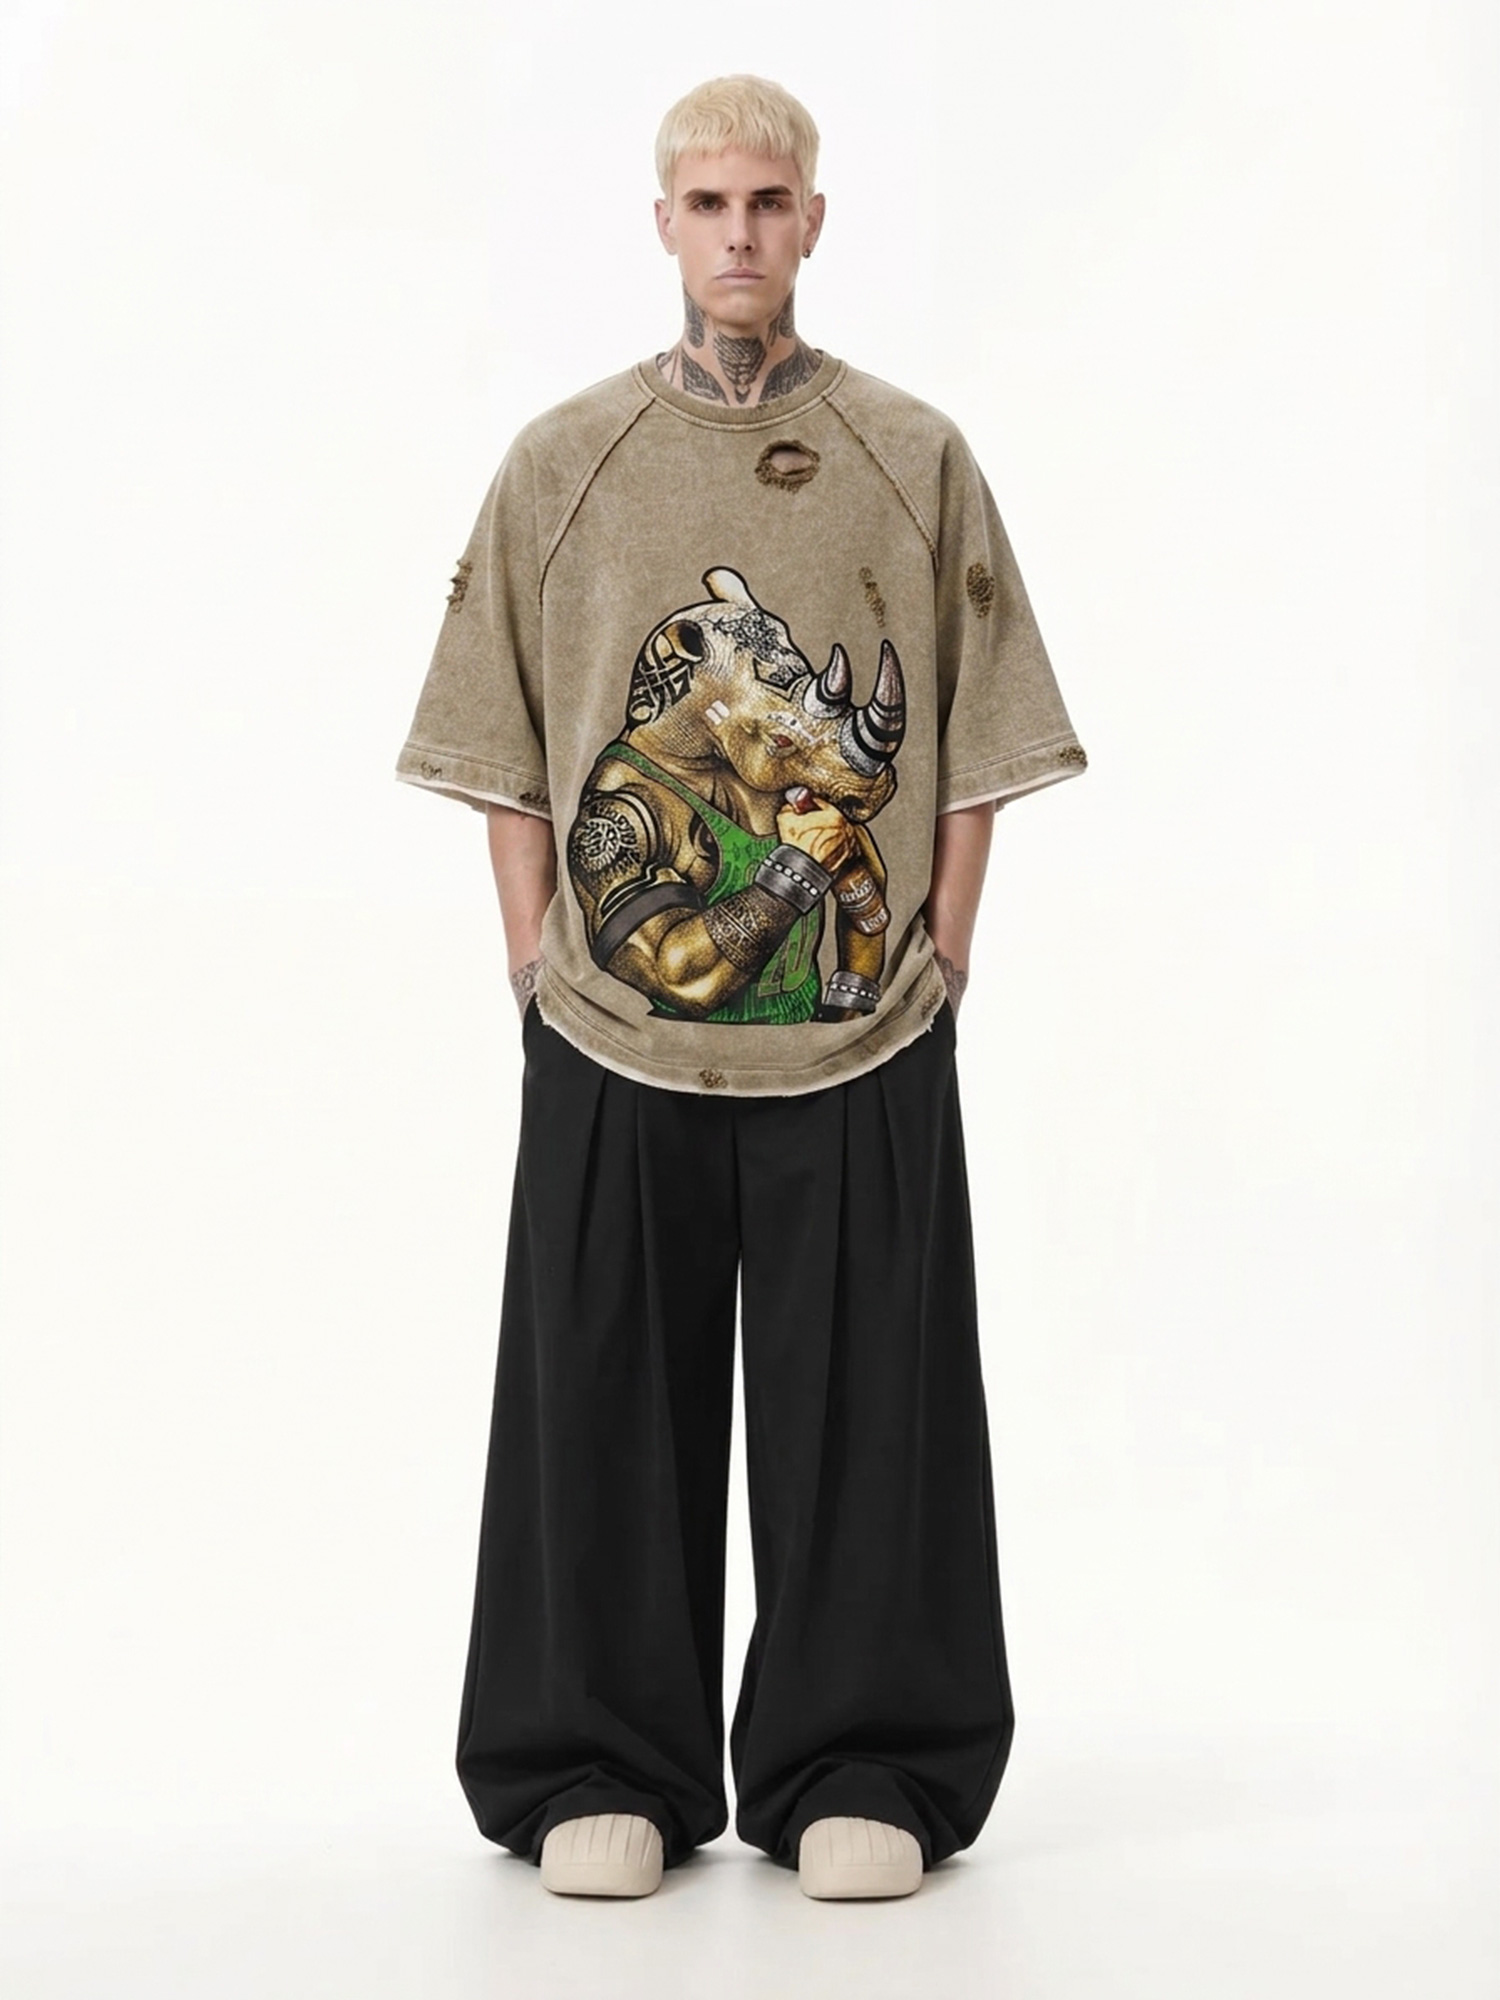
This molecular-level bonding prevents issues like surface cracking, peeling, or loss of fabric flexibility over time. Industry leaders like Dongguan City Dule Garment Co.,Ltd integrate advanced DTG digital printing into their end-to-end production ecosystem, seamlessly accommodating specialized techniques such as vintage washes, 3D embroidery, and puff printing on oversized drop-shoulder silhouettes.
Strategic Advantages for Modern Fashion Brands
- Eco-Friendly Chemical Profile: Formulated without phthalates or PVC, water-based inks significantly reduce volatile organic compound (VOC) releases during high-temperature curing cycles.
- Superior Breathability & Soft Touch: Direct pigment bonding preserves the original natural flexibility and air circulation of raw cotton fabrics.
- Optimized for Heavyweight Textiles: Performs exceptionally well on 480–630 GSM combed cotton, delivering crisp graphic resolution and vibrant color depth even after distressed wash treatments.
- Agile Supply Chain Support: Low minimum order quantities starting at 50 units for custom styles (and 20 units for blank tees) empower emerging apparel labels to test markets quickly.
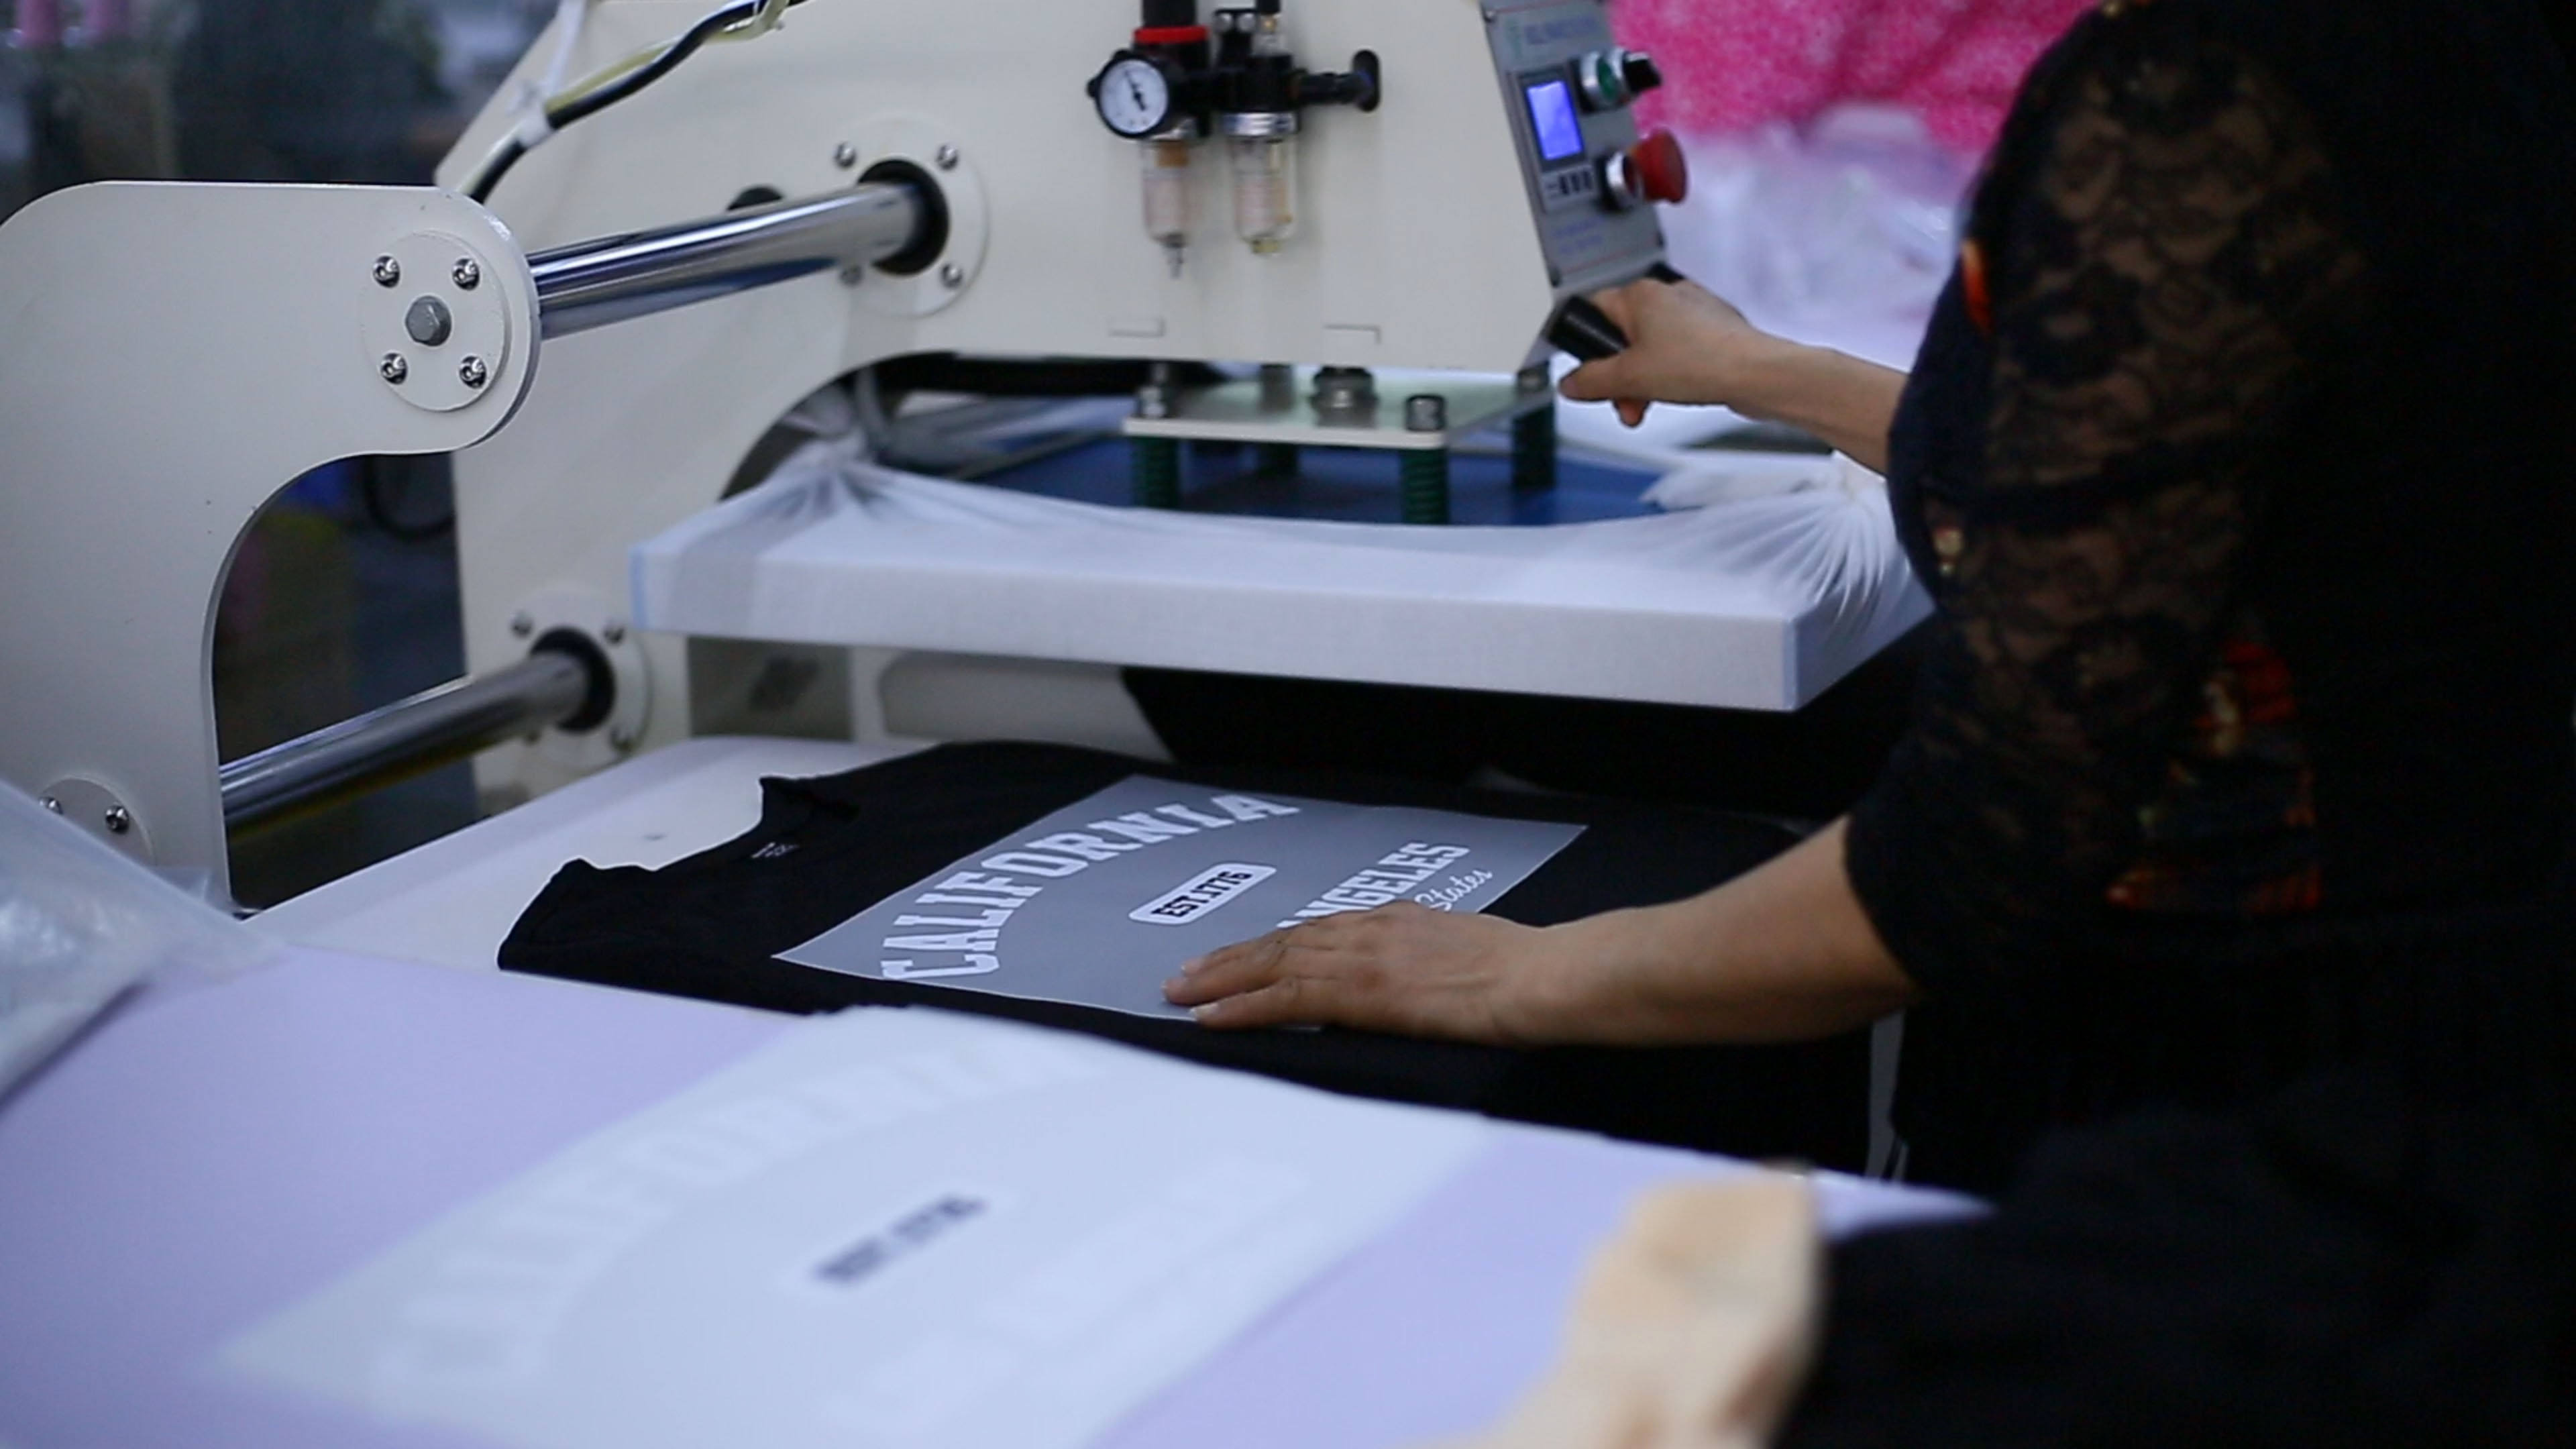
Such agile capabilities enable brands to implement fast-paced inventory strategies. For instance, UK fashion label Vanguard Shop Co. streamlined its operations by releasing 24 seasonal drops per year at 1,000 pieces per SKU, securing continuous bestseller restocks while drastically reducing unsold stock risk.
Comparative Analysis: Printing Techniques & Technical Specifications
The matrix below outlines key operational differences across major apparel printing methodologies and logistics parameters in garment manufacturing.
| Parameter / Metric | Water-Based DTG Printing | Plastisol Screen Printing | Sublimation Printing |
|---|---|---|---|
| Environmental Impact | Minimal (Eco-friendly, solvent-free) | High (Utilizes PVC & phthalates) | Moderate (Polyester restricted) |
| Touch & Hand-Feel | Ultra-soft, highly breathable | Dense, rigid plastic layer | Weightless, completely smooth |
| Textile Compatibility | 100% Cotton & Heavyweight Blends | Cotton, Poly-cotton Blends | 100% Synthetic / Polyester |
| Minimum Order Quantity (MOQ) | 50 pcs custom / 20 pcs blanks | High (typically 300+ units) | Moderate to High |
| Shipping & Trade Terms | FOB Shenzhen, DDP Door-to-Door | FOB Shenzhen, DDP Door-to-Door | FOB Shenzhen, DDP Door-to-Door |
Frequently Asked Questions
Are water-based prints durable through standard washing cycles?
Yes. When correctly cured and pre-treated, water-based pigment inks absorb into raw cotton fibers, achieving wash fastness rates that comply with international ISO standards without flaking or peeling over extended wear.
Which fabrics yield optimal print clarity with water-based inks?
100% combed natural cotton and premium heavyweight textiles (480–630 GSM) offer the highest color saturation, fine detail sharpness, and long-lasting durability.
What are the expected timelines for sampling and bulk manufacturing?
Sample creation takes between 3 to 15 days, while bulk production fulfillment typically ranges from 20 to 35 days based on fabric availability, custom washes, and design complexity.
Conclusion & Manufacturing Services
Integrating water-based DTG printing enables clothing brands to align market responsiveness with stringent environmental standards. Professional OEM and ODM services support versatile production schedules with low MOQs (50 pieces custom / 20 pieces blanks). Rigorous quality control protocols govern every stage, including pre-production sample approvals and final AQL 2.5 inspection according to ISO 2859-1 standards. Flexible shipping includes FOB Shenzhen, DDP Door-to-Door, Express (DHL/FedEx/UPS), and Sea Freight (FCL/LCL), with standard payment options such as Bank Transfer and Alipay. For technical consultations and orders, contact us at yutianfang88@gmail.com.
About Us
Dongguan City Dule Garment Co.,Ltd is an established OEM/ODM manufacturer specializing in custom streetwear and heavyweight apparel since 2007. Spanning a 5,000-square-meter facility with over 200 skilled staff, the company maintains robust in-house R&D capabilities, launching more than 500 original garment designs each year. Offering complete manufacturing solutions, the factory serves over 200 global apparel brands across North America, Europe, Australia, and Asia.
REPORT