




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
Why Injection Mould Samples Pass but Mass Production Parts Fail
A successful injection mould sample does not always guarantee reliable mass production. The trial may have been produced under carefully adjusted settings that cannot be maintained over hundreds or thousands of cycles. Variations in resin batches, machine performance, mould temperature, cooling, alignment, operator adjustments, and inspection practices can cause production parts to develop dimensional, surface, or assembly defects.
How to Prevent Production Failures
- Run the mould through multiple cycles to confirm repeatable performance instead of approving a single successful shot.
- Check material compatibility, mould alignment, cooling efficiency, dimensions, appearance, and part function before releasing the tool.
- Document sample approval requirements and continue inspections after production begins to detect process drift.
- Use the same validation approach for electronic housings, appliance components, automotive parts, and industrial plastic enclosures.
Why a Good Trial Sample Can Be Misleading
A mould trial demonstrates that the tool can make an acceptable part under a particular combination of resin, temperature, injection speed, pressure, holding conditions, cooling time, and machine settings. However, mass production adds repetition, longer running periods, material-lot changes, equipment differences, and possible operator intervention. Unless these factors are included in the validation plan, the approved sample may show only a short-term optimum rather than a stable manufacturing window.
Tooling issues may also become visible only after continuous production. Cooling imbalance can lead to warpage, while poor venting, inconsistent filling, or inadequate mould alignment may create flash, sink marks, dimensional variation, or registration errors. These risks are especially important for double shot and overmolding applications, where two materials and multiple moulding stages must work together accurately.
Controls for Double Shot and Overmolding Tools
The Custom Double Shot Overmolding Mold supplied by Longterm is designed for two-color injection structures and material combinations including ABS plus TPU and PP plus TPE. For this type of tooling, the validation process should confirm first-shot positioning, second-shot registration, material bonding, cavity filling, part dimensions, and surface condition. Longterm's stated inspection activities include mould trial runs, dimensional testing, and pre-shipment inspection.
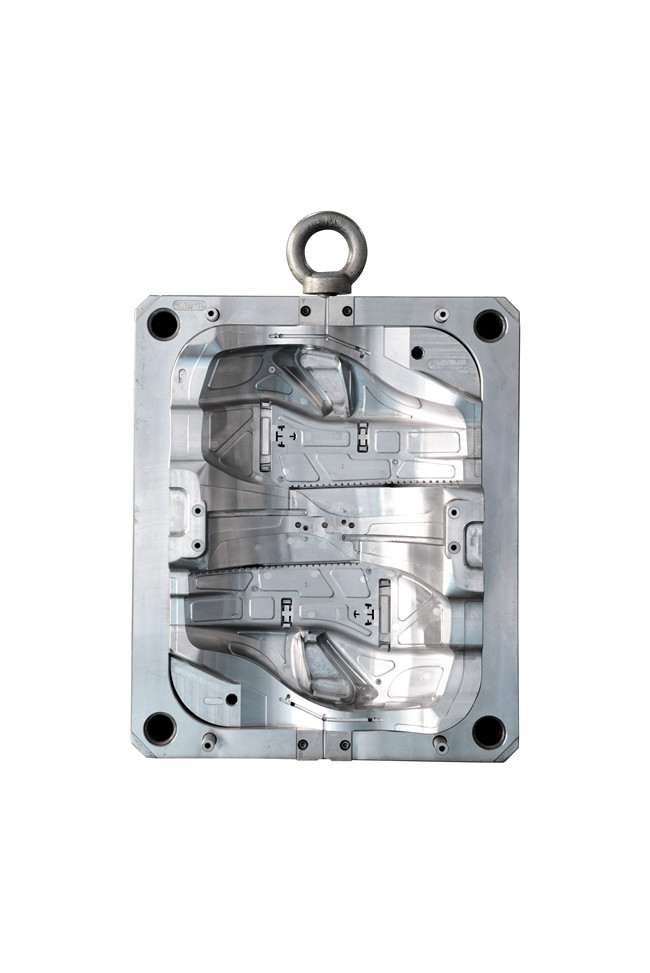
Approval should not end when the initial samples are signed off. Longterm describes a combination of first article inspection, complete dimensional measurement, mould running tests, CMM inspection, surface checks, multi-cycle trials, IQC, IPQC, and FQC. Each control addresses a separate stage of risk: incoming material quality, process consistency, tool performance, finished-part accuracy, appearance, and shipment release.
Production Validation Workflow
A practical release process begins with confirming the resin specification and checking incoming material. The mould should then be tested through enough consecutive cycles to expose temperature drift, cooling imbalance, wear, or unstable ejection. Critical dimensions can be measured using full inspection or CMM equipment, while visual areas require defined standards for texture, gloss, weld lines, flash, and other surface conditions.
For complex tools, signed sample approval should record the accepted material, machine parameters, cycle time, dimensions, appearance, and assembly requirements. Production teams can use these records as a reference when monitoring first-off parts and ongoing output. This makes it easier to identify changes caused by a new material lot, equipment adjustment, tool wear, or an uncontrolled process parameter.
Longterm reports experience with electronic housing moulds for an Italian manufacturer, double shot overmolding moulds for a French product brand, home appliance moulds for a US brand distributor, and an industrial plastic part mould for an Australian manufacturer. The reported customer feedback includes dimensional accuracy, surface quality, alignment, stable trial samples, technical problem solving, and delivery performance.
Longterm holds ISO 9001:2015 certification for the design, manufacturing, and sales of precision moulds and the sales of plastic products. This certification indicates a documented quality-management framework, while the company's trial, measurement, inspection, and sample-confirmation activities provide practical controls for tooling release and production follow-up.
Failure Cause and Recommended Control
| Production risk | Recommended validation or inspection |
|---|---|
| Trial settings work once but are not stable over repeated cycles | Multi-cycle mould trials and continuous mould running tests |
| Critical dimensions or alignment change during production | Full dimensional inspection, CMM measurement, and alignment verification |
| Resin batches or process conditions vary | IQC, IPQC, FQC, approved process records, and signed samples |
| Surface appearance becomes inconsistent | Defined surface inspection standards and production follow-up |
| Two-material parts show bonding or registration defects | Material compatibility checks, precise alignment checks, and multi-stage trial samples |
Frequently Asked Questions
Why might later injection moulded parts fail when the first sample passed?
The first sample may have been produced after manual optimization of the machine settings. During production, resin lots, barrel temperatures, cooling conditions, cycle times, machine behavior, or operator adjustments may change, causing the part to move outside the approved result.
What should be checked before a mould enters mass production?
Important checks include mould trial runs, multi-cycle stability, dimensional measurement, surface inspection, material verification, sample confirmation, and pre-shipment inspection. The exact inspection scope should reflect the part's critical dimensions, appearance requirements, material, and application.
Which checks are most important for double shot overmolding moulds?
Manufacturers should verify the first-shot and second-shot alignment, material compatibility, bonding performance, filling balance, mould running stability, dimensional accuracy, and final sample appearance. ABS plus TPU and PP plus TPE are among the material combinations supported by the listed double shot mould solution.
Conclusion
A good injection mould sample proves that acceptable results are possible, but it does not prove that the process will remain stable during mass production. Reliable release decisions require repeated-cycle mould trials, material and process verification, dimensional and surface inspection, documented sample approval, and production-stage monitoring. Longterm provides OEM custom plastic injection moulds, custom mould making with injection moulding, high-precision double shot and overmolding moulds, and mould development with plastic injection mass production. For detailed technical solutions or support, please reach out via rogerluo@longterm-mold.com.
About Longterm
Longterm Manufacturing Solutions Limited is a professional mould manufacturing company founded in 2010. It serves customers in the US, Europe, Australia, and other international markets through mould design, tooling, precision machining, mould manufacturing, and plastic parts production. The company has 50 employees and five R&D engineers with experience in injection mould structural design, precision CNC component solutions, sample verification, and manufacturing-process optimization. Longterm holds ISO 9001:2015 certification and has supported customers across several industries.
REPORT