




-
 Agriculture
-
 Health-Care
-
 Environment
-
 Construction-Real-Estate
-
 Tools-Hardware
-
 Home-Garden
-
 Furniture
-
 Luggage-Bags-Cases
-
 Medical-devices-Supplies
-
 Gifts-Crafts
-
 Sports-Entertainment
-
 Food-Beverage
-
 Vehicles-Transportation
-
 Power-Transmission
-
 Material-Handling
-
 Renewable-Energy
-
 Safety
-
 Testing-Instrument-Equipment
-
 Construction-Building-Machinery
-
 Pet-Supplies
-
 Personal-Care-Household-Cleaning
-
 Vehicle-Accessories-Electronics-Tools
-
 School-Office-Supplies
-
 Packaging-Printing
-
 Mother-Kids-Toys
-
 Business-Services
-
 Commercial-Equipment-Machinery
-
 Apparel-Accessories
-
 Security
-
 Shoes-Accessories
-
 Vehicle-Parts-Accessories
-
 Jewelry-Eyewear-Watches-Accessories
-
 Lights-Lighting
-
 Fabric-Textile-Raw-Material
-
 Fabrication-Services
-
 Industrial-Machinery
-
 Consumer-Electronics
-
 Electrical-Equipment-Supplies
-
 Electronic-Components-Accessories-Telecommunications
-
 Home-Appliances
-
 Beauty
-
 Chemicals
-
 Rubber-Plastics
-
 Metals-Alloys
































- Masonry Materials
- Curtain Walls & Accessories
- Earthwork Products
- Fireproofing Materials
- Heat Insulation Materials
- Plastic Building Materials
- Building Boards
- Soundproofing Materials
- Timber
- Waterproofing Materials
- Balustrades & Handrails
- Bathroom & Kitchen
- Flooring & Accessories
- Tiles & Accessories
- Door, Window & Accessories
- Fireplaces & Stoves
- Floor Heating Systems & Parts
- Stairs & Stair Parts
- Ceilings
- Elevators & Escalators
- Stone
- Countertops, Vanity Tops & Table Tops
- Mosaics
- Metal Building Materials
- Multifunctional Materials
- Ladders & Scaffoldings
- Mouldings
- Corner Guards
- Decorative Films
- Formwork
- Building & Industrial Glass
- Other Construction & Real Estate
- Wallpapers/Wall panels
- HVAC System & Parts
- Outdoor Facilities
- Prefabricated Buildings
- Festive & Party Supplies
- Bathroom Products
- Household Sundries
- Rain Gear
- Garden Supplies
- Household Cleaning Tools & Accessories
- Lighters & Smoking Accessories
- Home Storage & Organization
- Household Scales
- Smart Home Improvement
- Home Textiles
- Kitchenware
- Drinkware & Accessories
- Dinnerware, Coffee & Wine
- Home Decor
- Golf
- Fitness & Body Building
- Amusement Park Facilities
- Billiards, Board Game,Coin Operated Games
- Musical Instruments
- Outdoor Affordable Luxury Sports
- Camping & Hiking
- Fishing
- Sports Safety&Rehabilitation
- Ball Sports Equipments
- Water Sports
- Winter Sports
- Luxury Travel Equipments
- Sports Shoes, Bags & Accessories
- Cycling
- Other Sports & Entertainment Products
- Artificial Grass&Sports Flooring&Sports Court Equipment
- Scooters
- Food Ingredients
- Honey & Honey Products
- Snacks
- Nuts & Kernels
- Seafood
- Plant & Animal Oil
- Beverages
- Fruit & Vegetable Products
- Frog & Escargot
- Bean Products
- Egg Products
- Dairy Products
- Seasonings & Condiments
- Canned Food
- Instant Food
- Baked Goods
- Other Food & Beverage
- Meat & Poultry
- Confectionery
- Grain Products
- Feminie Care
- Hair Care & Styling
- Body Care
- Hands & Feet Care
- Hygiene Products
- Men's Grooming
- Laundry Cleaning Supplies
- Travel Size & Gift Sets
- Room Deodorizers
- Other Personal Care Products
- Pest Control Products
- Special Household Cleaning
- Floor Cleaning
- Kitchen & Bathroom Cleaning
- Oral Care
- Bath Supplies
- Yellow Pages
- Correction Supplies
- Office Binding Supplies
- Office Cutting Supplies
- Board Erasers
- Office Adhesives & Tapes
- Education Supplies
- Pencil Cases & Bags
- Notebooks & Writing Pads
- File Folder Accessories
- Calendars
- Writing Accessories
- Commercial Office Supplies
- Pencil Sharpeners
- Pens
- Letter Pad/Paper
- Paper Envelopes
- Desk Organizers
- Pencils
- Markers & Highlighters
- Filing Products
- Art Supplies
- Easels
- Badge Holder & Accessories
- Office Paper
- Printer Supplies
- Book Covers
- Other Office & School Supplies
- Stationery Set
- Boards
- Clipboards
- Stamps
- Drafting Supplies
- Stencils
- Electronic Dictionary
- Books
- Map
- Magazines
- Calculators
- Baby & Toddler Toys
- Educational Toys
- Classic Toys
- Dress Up & Pretend Play
- Toy Vehicle
- Stuffed Animals & Plush Toys
- Outdoor Toys & Structures
- Balloons & Accessories
- Baby Food
- Children's Clothing
- Baby Supplies & Products
- Maternity Clothes
- Kids Shoes
- Baby Care
- Novelty & Gag Toys
- Dolls & Accessories
- Puzzle & Games
- Blocks & Model Building Toys
- Toddler Clothing
- Baby Clothing
- Kids' Luggage & Bags
- Arts, Crafts & DIY Toys
- Action & Toy Figures
- Baby Appliances
- Hobbies & Models
- Remote Control Toys
- Promotional Toys
- Pregnancy & Maternity
- Hygiene Products
- Kid's Textile&Bedding
- Novelty & Special Use
- Toy Weapons
- Baby Gifts
- Baby Storage & Organization
- Auto Drive Systems
- ATV/UTV Parts & Accessories
- Marine Parts & Accessories
- Other Auto Parts
- Trailer Parts & Accessories
- Auto Transmission Systems
- Train Parts & Accessories
- Universal Parts
- Railway Parts & Accessories
- Auto Brake Systems
- Aviation Parts & Accessories
- Truck Parts & Accessories
- Auto Suspension Systems
- Auto Lighting Systems
- New Energy Vehicle Parts & Accessories
- Auto Steering Systems
- Wheels, Tires & Accessories
- Bus Parts & Accessories
- Auto Performance Parts
- Cooling System
- Go-Kart & Kart Racer Parts & Accessories
- Air Conditioning Systems
- Heavy Duty Vehicle Parts & Accessories
- Auto Electrical Systems
- Auto Body Systems
- Auto Engine Systems
- Container Parts & Accessories
- Motorcycle Parts & Accessories
- Refrigeration & Heat Exchange Equipment
- Machine Tool Equipment
- Food & Beverage Machinery
- Agricultural Machinery & Equipment
- Apparel & Textile Machinery
- Chemical Machinery
- Packaging Machines
- Paper Production Machinery
- Plastic & Rubber Processing Machinery
- Industrial Robots
- Electronic Products Machinery
- Metal & Metallurgy Machinery
- Woodworking Machinery
- Home Product Manufacturing Machinery
- Machinery Accessories
- Environmental Machinery
- Machinery Service
- Electrical Equipment Manufacturing Machinery
- Industrial Compressors & Parts
- Tobacco & Cigarette Machinery
- Production Line
- Used Industrial Machinery
- Electronics Production Machinery
- Other Machinery & Industrial Equipment
- Camera, Photo & Accessories
- Portable Audio, Video & Accessories
- Television, Home Audio, Video & Accessories
- Video Games & Accessories
- Mobile Phone & Accessories
- Electronic Publications
- Earphone & Headphone & Accessories
- Speakers & Accessories
- Smart Electronics
- TV Receivers & Accessories
- Mobile Phone & Computer Repair Parts
- Chargers, Batteries & Power Supplies
- Used Electronics
- VR, AR, MR Hardware & Software
- Projectors & Presentation Equipments
- Other Consumer Electronics
- Cables & Commonly Used Accessories
- Computer Hardware & Software
- Displays, Signage and Optoelectronics
- Discrete Semiconductors
- Wireless & IoT Module and Products
- Telecommunications
- Connectors, Terminals & Accessories
- Development Boards, Electronic Modules and Kits
- Circuit Protection
- Sensors
- Isolators
- Audio Components and Products
- Integrated Circuits
- Power Supplies
- Relays
- RF, Microwave and RFID
- Electronic Accessories & Supplies
- Passive Components
- PCB & PCBA
- Air Quality Appliances
- Home Appliance Parts
- Heating & Cooling Appliances
- Small Kitchen Appliances
- Laundry Appliances
- Water Heaters
- Water Treatment Appliances
- Refrigerators & Freezers
- Personal Care & Beauty Appliances
- Major Kitchen Appliances
- Cleaning Appliances
- Second-hand Appliances
- Smart Home Appliances
- Other Home Appliances
- Energy Chemicals
- Inorganic Chemicals
- Basic Organic Chemicals
- Agrochemicals
- Admixture & Additives
- Catalysts & Chemical Auxiliary Agents
- Pigments & Dyestuff
- Coating & Paint
- Daily Chemicals
- Polymer
- Organic Intermediate
- Adhesives & Sealants
- Chemical Waste
- Biological Chemical Products
- Surface Treatment Chemicals
- Painting & Coating
- Chemical Reagents
- Flavor & Fragrance
- Non-Explosive Demolition Agents
- Other Chemicals
- Custom Chemical Services
How to Successfully File a Claim for Leaking Pipe Fittings Post-Installation
Discovering fluid leakage in pipe fittings after installation can lead to costly operational downtime and system failure. To successfully claim compensation or replacements from a supplier, buyers must compile a comprehensive evidentiary package. Demonstrating that the leak stems from manufacturing non-conformity rather than field assembly errors requires clear documentation, technical inspection records, and precise operational logs.
Key Steps for Gathering Claim Evidence
- Visual & Live Media Evidence: Document the exact point of leakage with high-definition video and photo records under active pressure before disassembling the connection.
- Assembly & Operating Logs: Maintain detailed records of installation torque, sealing tape or compound application, pressure levels, and environmental conditions during failure.
- Traceability & Material Proof: Retain purchase orders, batch numbers, and mill test reports confirming raw material compliance (e.g., 304 or 316L stainless steel).
- Dimensional & Engineering Reports: Obtain technical inspection data comparing component measurements against engineering tolerances (such as ±0.03mm standards).
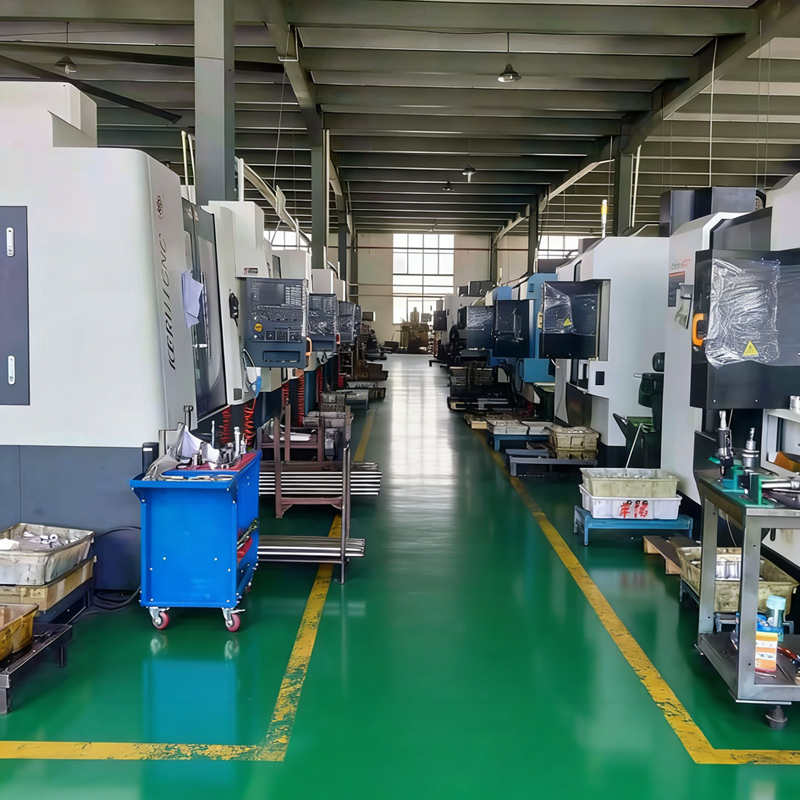
Technical Root Cause Analysis: Factory Defect vs. Field Error
When a fluid handling component fails in service, manufacturers evaluate whether the issue originated in the factory or during field installation. Components deployed in pipeline networks, marine equipment, or food processing lines experience significant mechanical stress. Proving a vendor's liability requires establishing an uninterrupted link between the failure mechanism and factory production parameters.
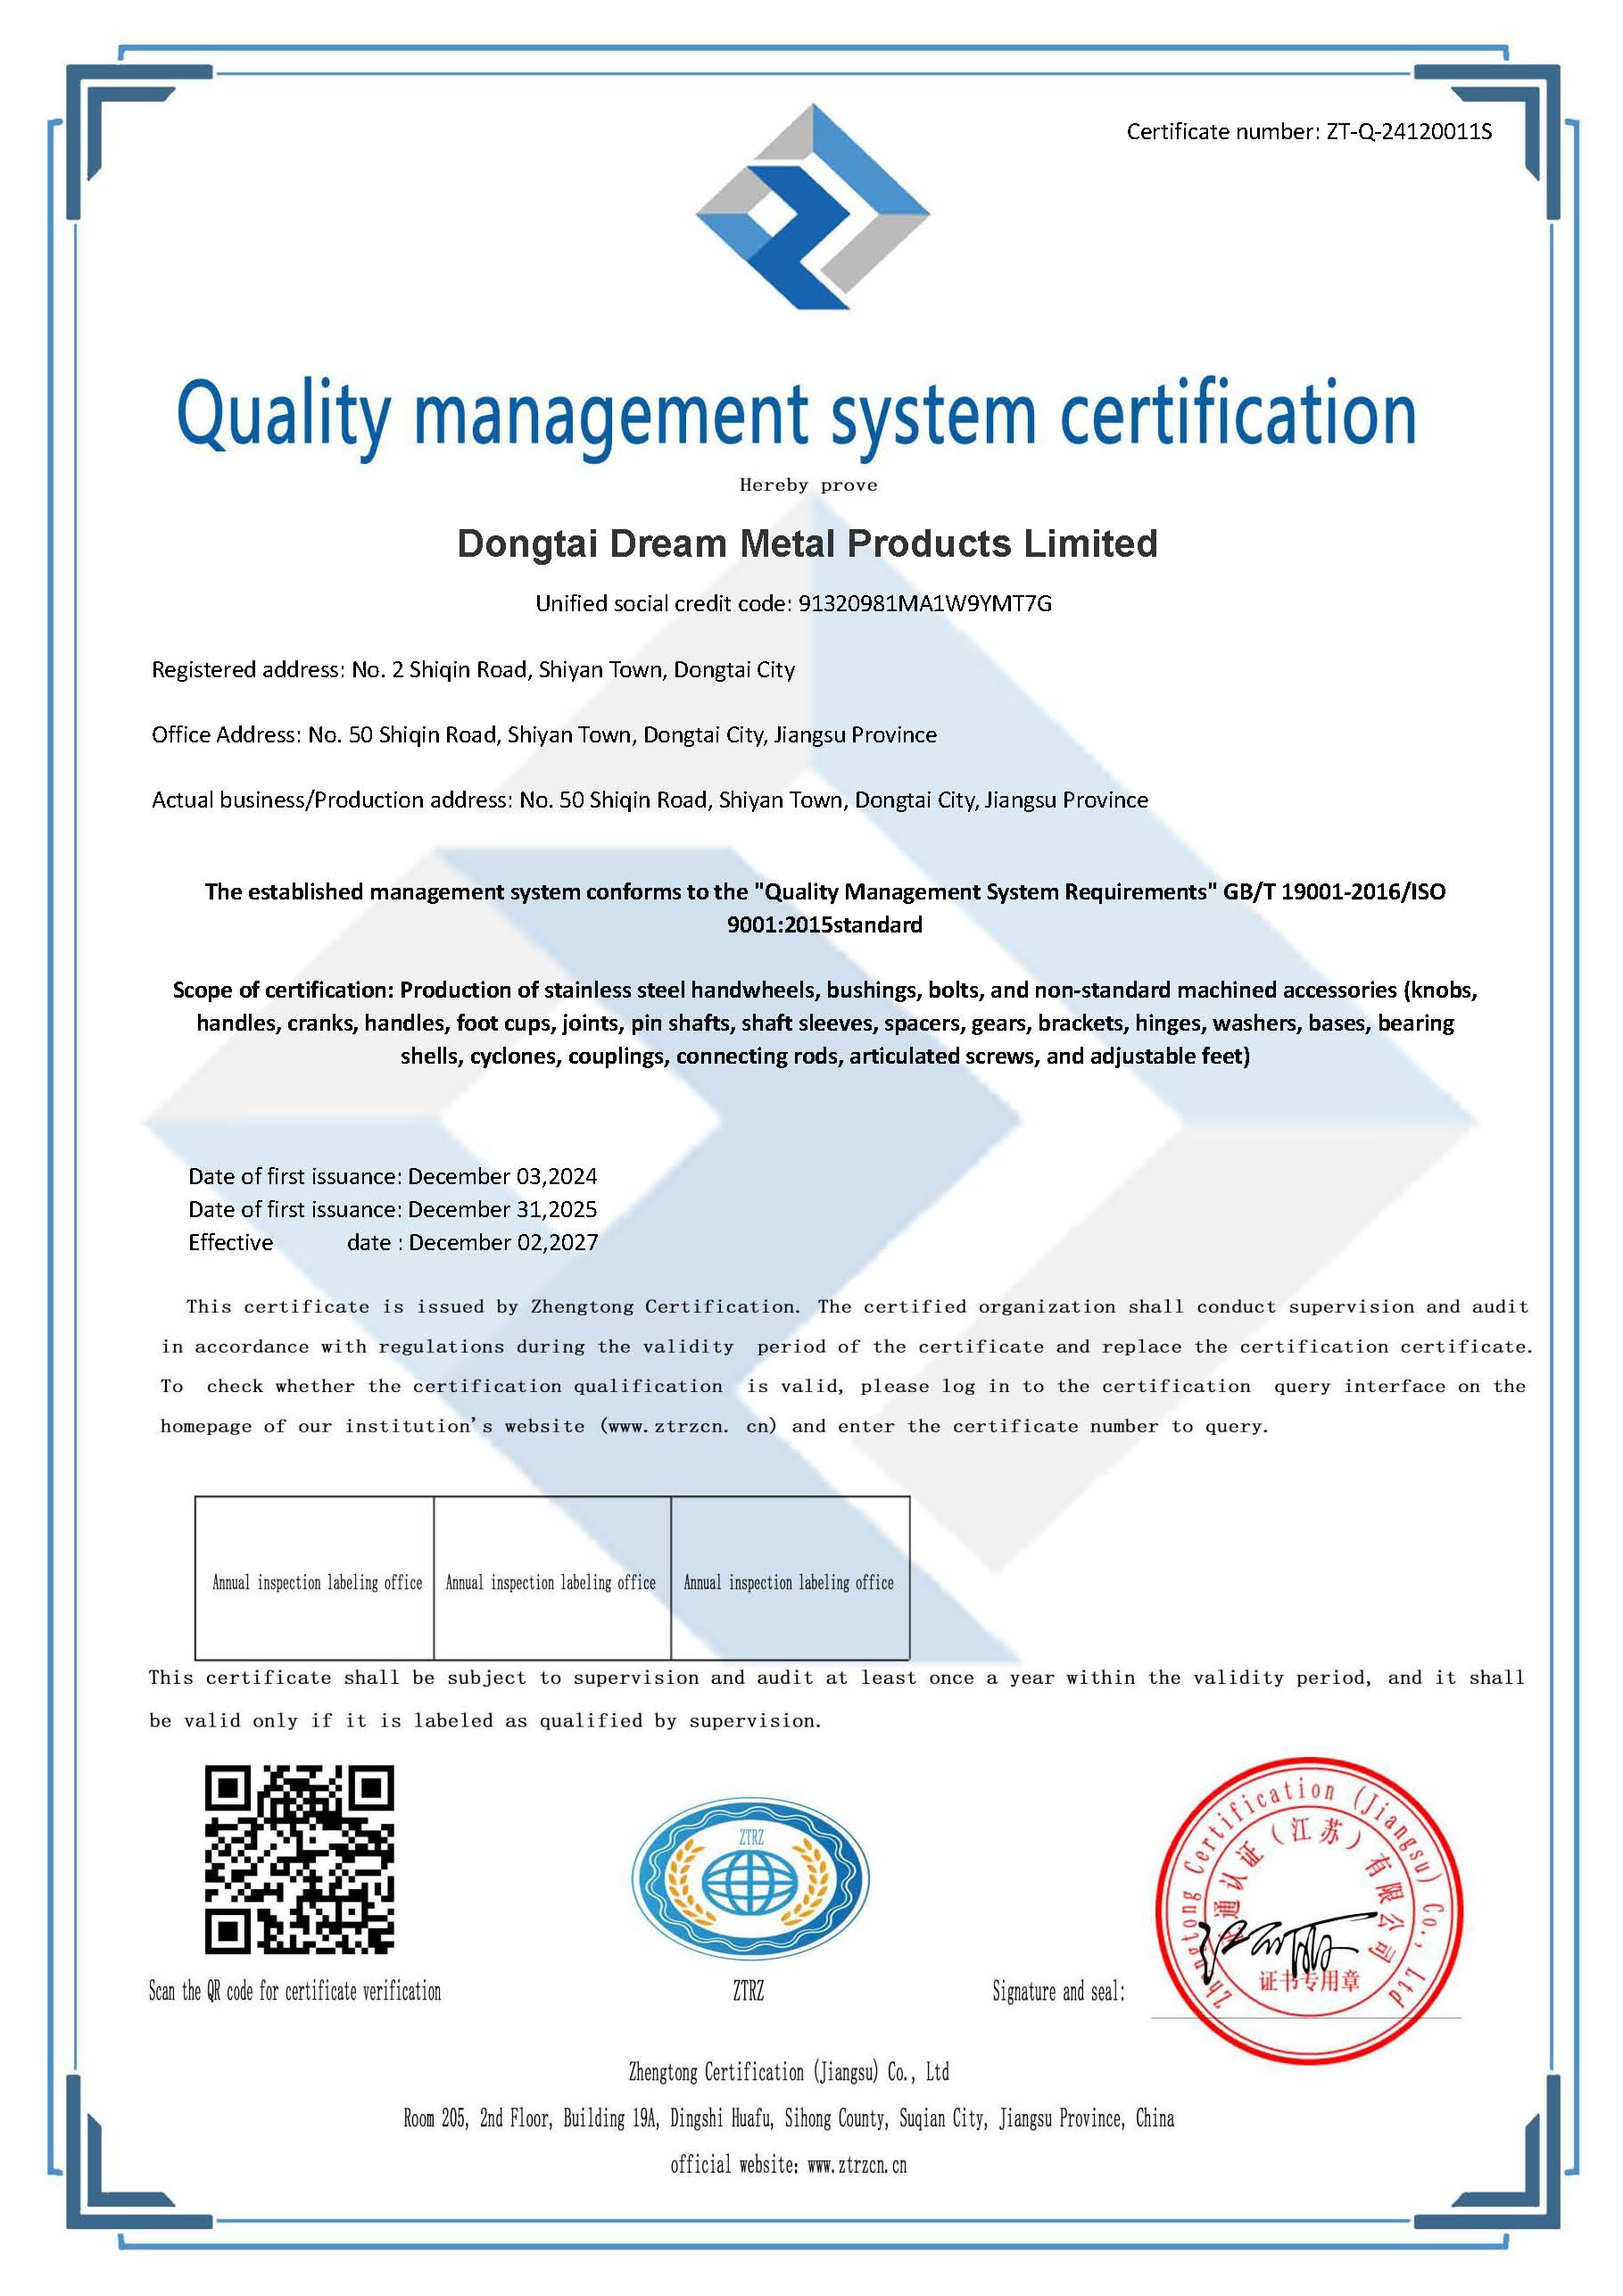
Material non-conformity—such as chemical imbalances, internal porosity, or improper heat treatment leading to stress corrosion cracking—can be verified through independent laboratory testing. Furthermore, ISO 9001 certified facilities (like certificate ZT-Q-24120011S) adhere to strict dimensional controls. If a coordinate measuring machine (CMM) report shows thread pitch deviation, depth errors, or sealing angle variances exceeding standard ±0.03mm limits, responsibility falls on the manufacturer.
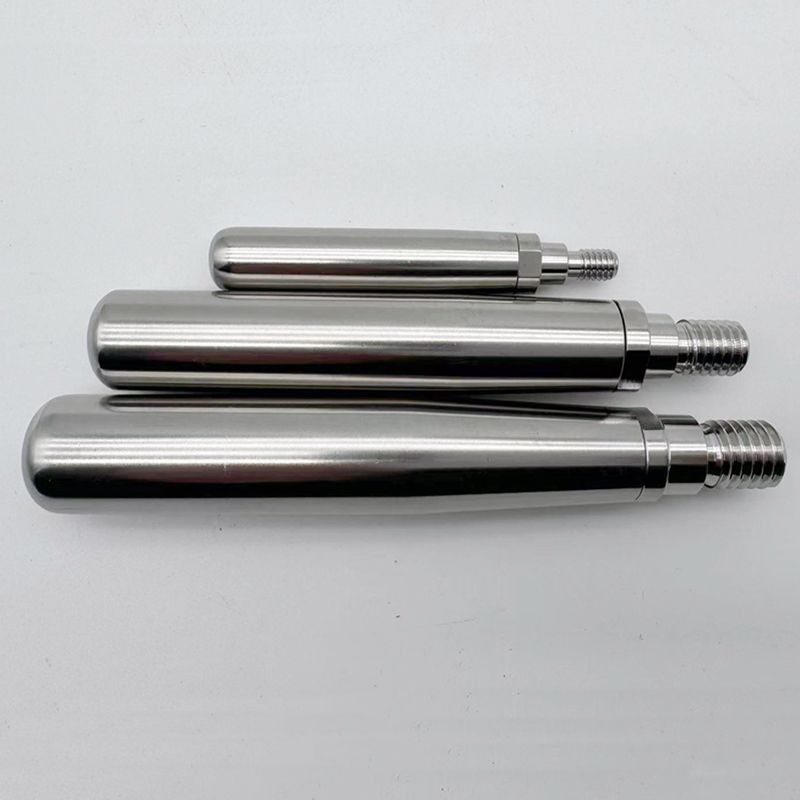
Conversely, field operational logs must prove that system pressure did not exceed component specifications during commissioning. For instance, in an industrial order involving 8,000 valve units, pressure monitoring charts serve as essential proof that operating thresholds were respected.
Evidence & Verification Matrix by Cause of Failure
The matrix below outlines the documentation required to substantiate claims based on specific failure categories.
| Defect Category | Required Evidence Package | Verification Technique | Claim Approval Likelihood |
|---|---|---|---|
| Thread / Machining Imperfection | Pitch gauge photos, overlay against engineering drawings, CMM report | Tolerance verification (beyond ±0.03mm variance), optical comparator testing | High (Manufacturing Defect) |
| Material Porosity / Void | Hydrostatic test video under static load, metallurgical lab report | Spectrometer material composition test, pressure bench validation | High (Material Non-Conformance) |
| Over-Torquing / Improper Assembly | Missing torque wrench records, stripped or deformed thread photos | Fractographic analysis indicating shear stress from excess torque | Low (Field Installation Mistake) |
| Chemical Attack / Corrosion | Fluid analysis sheet, temperature logs, pitting imagery | Corrosion product analysis compared against 304/316L alloy standards | Conditional (Material Selection Issue) |
Frequently Asked Questions
What media records should be taken immediately upon finding a leak?
Record wide-angle video showing the entire piping arrangement, mid-range shots showing batch numbers and part markings, and close-ups of the leak point while under line pressure. Include active pressure gauge readings within the frame.
Why are raw material test reports crucial for leakage claims?
Material certificates verify that the fitting meets specified alloy requirements, such as 316L stainless steel for corrosive environments. If lab tests reveal chemical composition deviations, the supplier is liable for premature failure or corrosion.
How do suppliers handle validated batch defect claims?
Upon confirming manufacturing defects through technical reports, suppliers typically issue a root-cause analysis (RCA), dispatch rapid replacement units, or provide financial credit to minimize operational disruption.
Summary & Procurement Recommendations
To resolve post-installation leakage claims quickly, procurement teams must present structured technical evidence that isolates manufacturing flaws from assembly errors. Implementing clear quality control checks upon delivery and relying on standardized OEM/ODM contracts ensures transparent claim resolution. For technical support or product inquiries, contact our team directly at 86-15868979792.
About Us
ZheJiang Dream Industry Limited (brand MXCZ) brings over two decades of expertise in custom CNC machining and precision mechanical engineering. Founded in 2008, the company operates a 2,500 sqm production facility with 34 skilled staff members dedicated to custom milling, turning, and assembly. Operating under ISO 9001 certification (ZT-Q-24120011S), the business exports 65% of its precision hardware to over 30 countries across industrial valve, marine, and automation industries.
REPORT